Waterproof Cable Gland
Waterproof Split Cable Glands Guide
Discover waterproof split cable glands with IP66 IP68 ratings nylon brass stainless steel options ideal for pre-terminated cable installations and retrofitting.
Read More
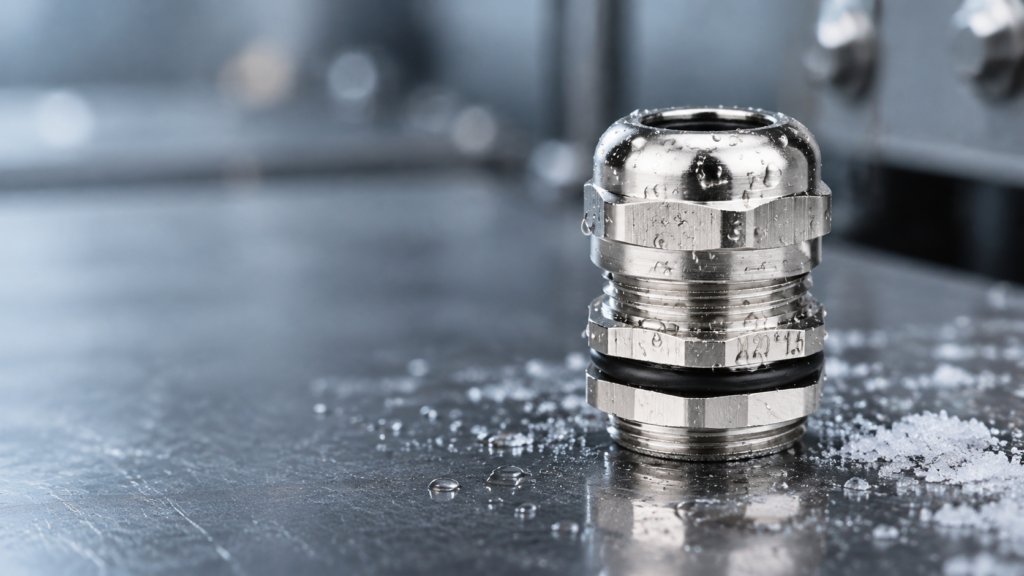
A nickel plated brass cable gland is a machined or forged brass body with a thin electrodeposited nickel layer over the whole surface. The layer is measured in micrometres, it follows the machined profile including the threads, and it is applied after machining rather than before.
That last point matters more than it sounds. Because the coating goes on last, it covers the thread flanks as well as the flats, and it is thinnest exactly where the geometry concentrates current during plating: the crests of the threads and the sharp machined edges. Understanding that distribution explains most of what follows about how plating performs and how it fails.
Two processes dominate. Electroplated nickel uses a current to deposit metal and gives a bright finish quickly; electroless nickel deposits chemically, covers recesses and thread roots more evenly and is harder, at higher cost. For a cable gland the practical difference appears at the thread crests, where electroplating is thinnest, and in the recesses, where electroless holds its thickness. Ask which process is used before comparing two quotations on price alone, because they are not the same product.
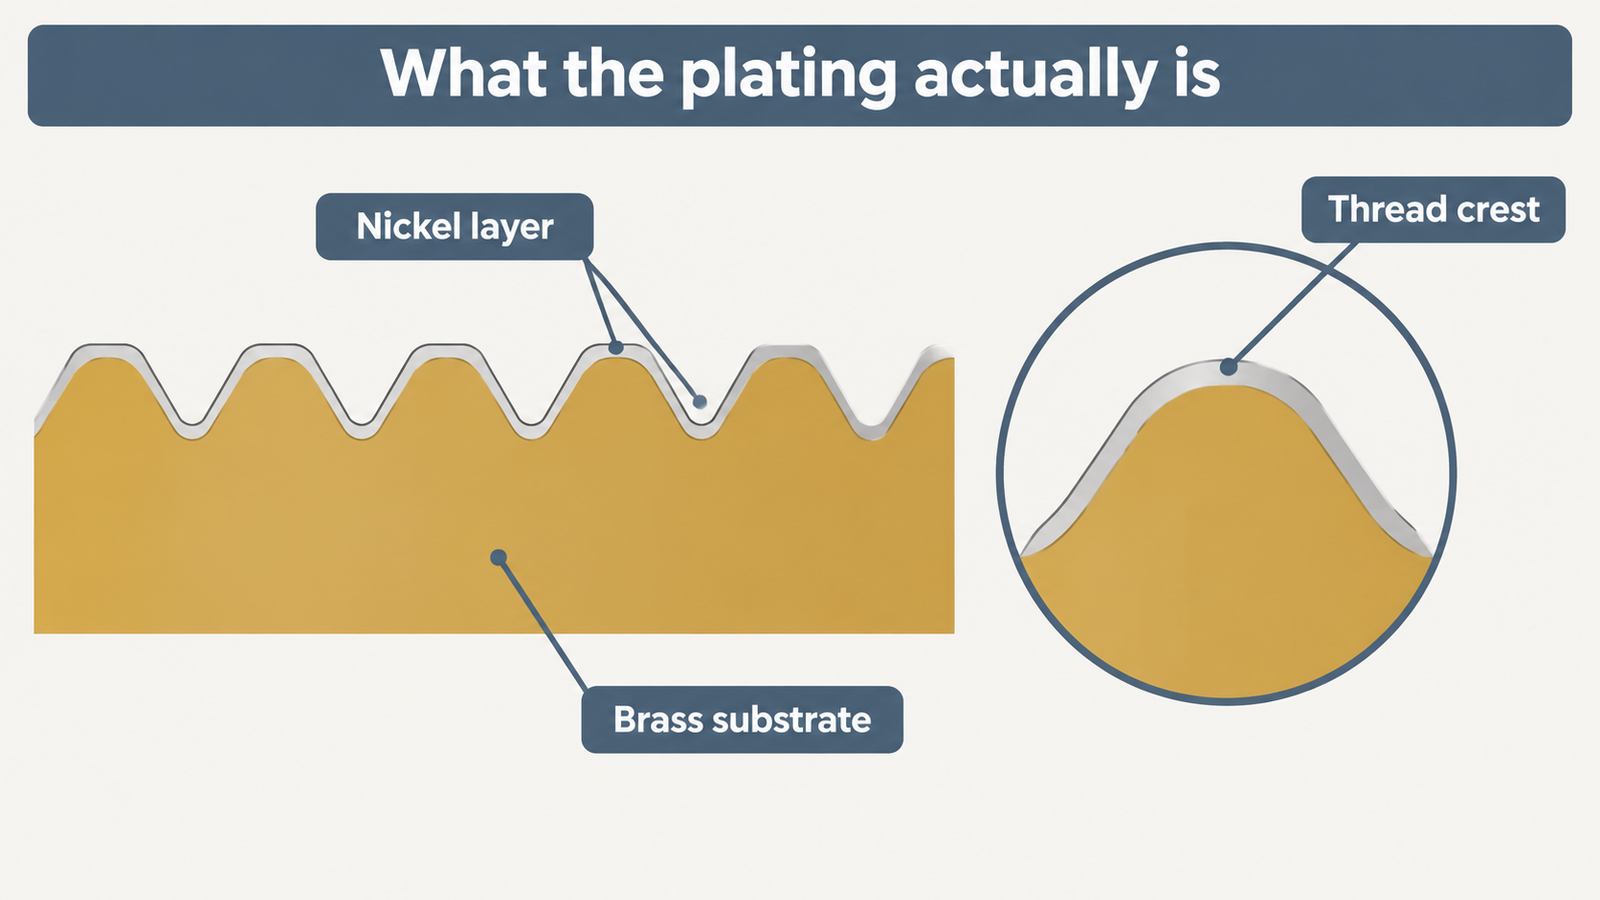
Plating is a barrier, and a barrier is a limited promise. Suppliers who describe it as corrosion protection without qualification are describing the good case only.
| Plating does | Plating does not |
|---|---|
| Separates the brass from the atmosphere and slows tarnishing | Change the alloy underneath or its mechanical limits |
| Gives a harder surface that resists light abrasion and handling marks | Survive deep scratches, cut edges or thread damage |
| Keeps visible outdoor equipment looking serviceable for longer | Make brass suitable for continuous chloride or ammonia exposure |
| Reduces friction on threads compared with bare brass | Raise the temperature rating, which is set by the elastomer |
The most misunderstood item is the last row of the left column. Bright, consistent appearance is evidence of a well-controlled plating process, not evidence of corrosion performance. Two glands can look identical on a bench and behave very differently after a year outdoors.
This is the point where the brass cable gland range deserves a closer look than a photograph. The catalogue image shows the finish; it cannot show the thickness, the adhesion or the salt spray criterion behind it, and those are the three properties that decide how the gland looks in five years.
Plating thickness is the single specification that separates a finish description from a finish requirement. A quotation that says “nickel plated” states a process; it does not state how much nickel is present, and without that number there is nothing to inspect against.
| What to ask | Why it changes the answer |
|---|---|
| Minimum thickness in micrometres | A minimum is an acceptance criterion; an average is not |
| On which surface the figure applies | Thread crests plate thinner than flats, and crests are where wear starts |
| Which measurement method | X-ray fluorescence, coulometric and microscopy give different numbers |
| Whether it is per batch or per sample | A single coupon does not describe a production lot |
Industrial nickel plating on brass hardware generally sits in the single-digit to low-double-digit micrometre range, with heavier deposits used where abrasion or chemical exposure is expected. The exact figure is the supplier’s to declare. What matters for the buyer is that a figure exists, applies to a defined surface and comes with a method.
Salt spray hours are the most quoted and least comparable figure in cable gland marketing. A number without a standard, a corrosion criterion and a test specimen description tells you very little.
Three questions turn a claim into information. First, which standard: neutral salt fog testing to ASTM B117 or ISO 9227 is the usual reference, and accelerated tests are not service-life predictions. Second, which failure point: hours to white corrosion of the coating is a different number from hours to base metal corrosion, and the second is the one that matters for structural integrity. Third, was the specimen scribed or damaged before testing, because a scribed sample tests the coating’s ability to protect a breach rather than its ability to stay intact.
A supplier who can answer all three is describing a tested product. A supplier who quotes a large number and nothing else is describing a brochure.
It is also worth remembering what a salt fog chamber does not reproduce. It holds one temperature, one salt concentration and a continuous wet condition, which is harsher than a sheltered industrial site in some ways and much easier than a coastal one in others. Use the result to compare finishes against each other, not to estimate years of service.
| Environment | Reasonable finish | Reasoning |
|---|---|---|
| Indoor cabinet, dry, not visible | Unplated brass | Plating adds cost and buys nothing indoors |
| Indoor, visible equipment, showroom panels | Nickel plated | Appearance retention is the actual requirement |
| Sheltered outdoor, occasional rain | Nickel plated | Barrier plus harder surface for handling and cleaning |
| Exposed outdoor, industrial atmosphere | Nickel plated, inspected | Works if the coating stays intact; damage is the failure mode |
| Coastal, marine, continuous chloride | Stainless steel | Plating is a barrier that chlorides eventually breach |
| Washdown with chlorinated or caustic cleaners | Stainless steel | Chemistry attacks the coating and then the brass |
The dividing line is not indoor versus outdoor. It is whether the coating can reasonably be expected to stay continuous for the service life of the installation. Where mechanical damage is likely and the environment is aggressive at the same time, plating is the wrong tool regardless of thickness.
Almost every plating failure in service begins as mechanical damage during installation, not as a chemical attack on an intact coating.
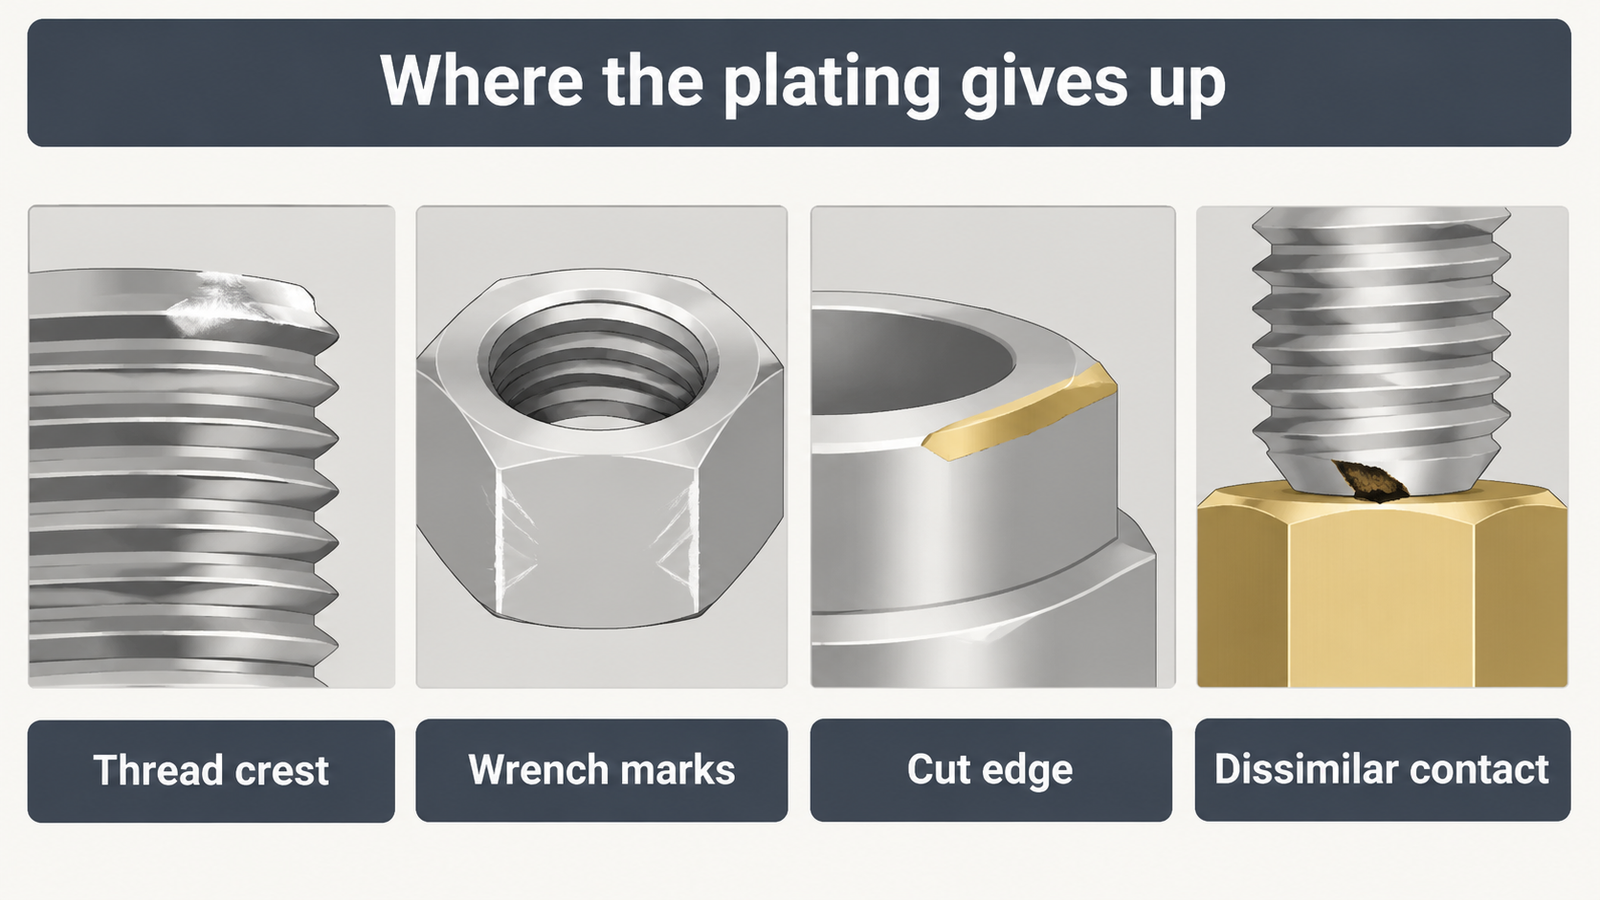
Thread crests wear as the gland is run in and out, and a gland that has been fitted twice already has exposed brass on its most highly stressed surface. Wrench marks are the most visible and the most avoidable: a correctly sized spanner or a strap wrench leaves the coating intact, while grips and pipe wrenches do not. Cut edges from machining or from trimming a thread expose the substrate along a line, which is a far more effective starting point for corrosion than a round scratch. Dissimilar contact, particularly against aluminium, sets up a small galvanic couple at the joint that keeps the exposed area active.
The practical consequence is that plating quality and installation discipline cannot be separated. A heavier coating survives rougher handling, but no coating survives a pipe wrench.
| Finish | Strength | Limitation |
|---|---|---|
| Unplated brass | Cheapest, no coating to damage, natural patina | Tarnishes quickly, appearance degrades, no abrasion benefit |
| Nickel | Hard, bright, good barrier, widely available | Thin at crests and edges; obvious when damaged |
| Chrome over nickel | Harder and brighter still | Brittle deposit, can flake at edges, rarely needed on glands |
| Zinc | Sacrificial protection on steel | Not the usual finish for brass bodies |
| Tin | Soft, good contact resistance | Wears quickly on threads |
| Epoxy or powder coat | Thick barrier, colour options | Thickness bridges threads; damage is hard to see |
For most industrial work the real choice is between unplated brass, nickel plated brass and stainless steel. The middle option is the right one more often than either extreme, provided the specification includes a thickness figure.
Four conditions should end the plating discussion. Continuous chloride exposure, including coastal air and marine decks. Washdown with chlorinated water or caustic cleaners. Immersion or frequent standing water. And sustained temperatures above the elastomer rating, where the seal rather than the body becomes the limit.
In each case the answer is a different body material, not a thicker coating. The stainless steel range covers the sizes that replace plated brass directly, and the brass gland guide explains where the brass family as a whole stops being appropriate.
One related decision is easy to overlook: on an entry that is both wet and exposed, the finish is not the only variable. The number of seals the gland carries often matters more than the coating on its body, and BW vs CW cable glands sets out how to decide that for a given location.
| Line | What to write |
|---|---|
| 1 | Nickel plated brass, with the minimum thickness in micrometres and the surface it applies to |
| 2 | The measurement method accepted for inspection |
| 3 | Salt spray requirement, with the standard, the corrosion criterion and whether the specimen is scribed |
| 4 | Appearance acceptance: no bare brass on thread crests, no blistering or flaking |
| 5 | Packing that protects the coating in transit, since bag abrasion damages threads |
Five lines are enough to make the finish inspectable at goods-in, which is the only point where a plating problem is cheap to resolve.
The check itself takes seconds per box: look at the thread crests of a sample, look for blistering on the flats and look at the machined edges. Bare brass at a crest on a brand-new part is not normal wear, it is a plating defect, and it is worth rejecting at receipt rather than explaining to a client eighteen months later. Where the installation also has to meet a sealing requirement, the IP rating guide explains how finish and sealing class are assessed together.
Plating adds a small per-piece cost rather than a step change, so nickel plated standard sizes sit at the upper part of the standard brass band rather than in a separate price class. Standard brass glands typically run from about US$0.08 to US$1.20 depending on size, with plated versions quoted at the upper end; EMC versions run from about US$0.90 to US$6.50 and Ex versions from about US$2.50 to US$14.00. These are indicative FOB Ningbo or Shanghai prices at 1,000 pieces per size for brass and 300 pieces per size for Ex.
Minimum order quantity for brass, plated or not, is normally 1,000 pieces per size with no tooling charge, and trial orders of 100 to 500 pieces are usually accepted at a higher unit price. Because plating is applied per batch, changing the finish after the order is placed means re-running the batch, which is why the finish belongs in the first enquiry rather than the last email.
Discover waterproof split cable glands with IP66 IP68 ratings nylon brass stainless steel options ideal for pre-terminated cable installations and retrofitting.
Read More
Zone 1 and Zone 2 cable glands are selected from the area classification, not the catalogue. See how the zone sets the minimum EPL, what the gland marking must show, and the mistakes to avoid.
Read More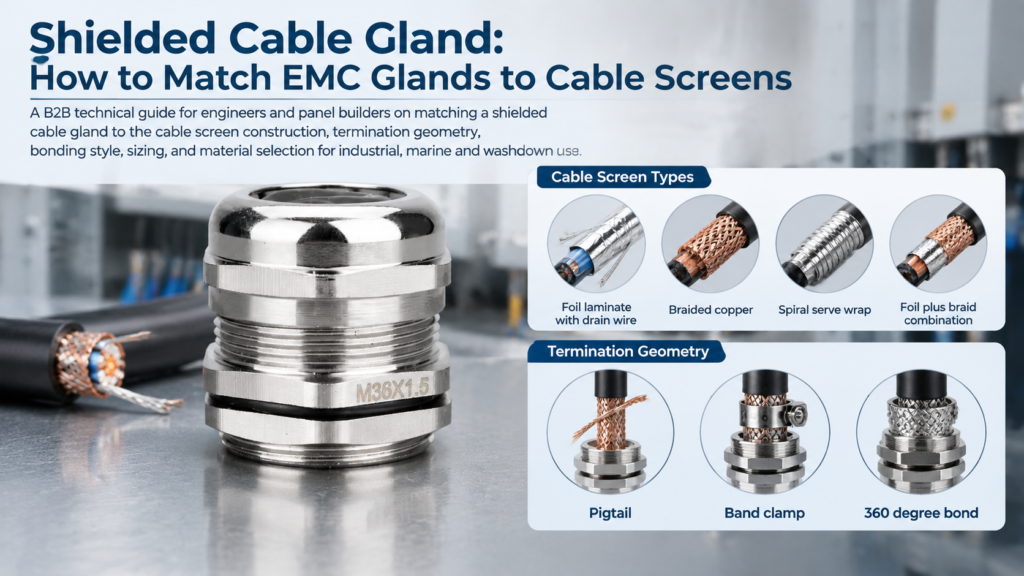
Match an EMC cable gland to the cable screen: foil, braid, spiral and combination constructions, termination geometry, bonding rules and sizing on jacket OD.
Read More