A chemical plant does not fail a cable gland with one dramatic event. It fails it slowly: a brown stain at a thread root in month four, a pinhole in the body in year two, a crust of crystallised product bridging the seal. By the time anyone writes a work order, the alloy decision that caused it was made three years earlier on a requisition that said only “stainless”.
This page is about that decision, narrowed to one grade. If you are still deciding whether stainless is needed at all, the media-driven method in our chemical resistant cable gland guide is the right starting point. What follows assumes the question is now: which stainless, and how does it survive contact with the plant.
316L Is the Floor of the Conversation, Not the Ceiling
In practice 316L is where chemical plant specifications start, which creates false confidence. The L means low carbon, capped at 0.03 percent, and its purpose is to stop chromium carbide precipitating at grain boundaries during welding. A gland body is not welded, so the L adds little to the body itself; it matters for the plate the gland threads into and for a welded bracket or skid repair.
What 316L really buys you is molybdenum: two to three percent Mo is what lets an austenitic stainless resist pitting in chloride-bearing water, a genuine step up from 304. It is not a universal answer. Failures here are almost always the wrong grade for the media family, the right grade with a crevice nobody designed out, or the right grade contaminated on site.
Media Family to Grade Boundary
The useful way to think about compatibility is at family level, then verify at the actual concentration and temperature. A gland that is correct for dilute caustic at ambient temperature can be wrong for the same chemical hot and concentrated, and no brochure will tell you.
Media family
316L verdict
What the plant should do instead
Dilute mineral acids, cold, intermittent splash
Acceptable, with margin
Confirm by coupon test or supplier immersion data before specifying across a line
Concentrated sulphuric acid
Conditional, depends heavily on concentration and temperature
Do not generalise from one successful line to another; specify per stream
Hydrochloric acid, any concentration
Not acceptable
Non-metallic body, or a lined and isolated entry; no stainless grade rescues this
Hydrofluoric acid and fluorinated media
Not acceptable
Same as above; also review the seal elastomer separately
Caustic soda and caustic potash
Generally good, but stress corrosion cracking becomes the risk at temperature
Check for residual stress in the fitting and avoid hot concentrated service without review
This is the single most common mistake in CIP chemical selection
Solvents, oils, most hydrocarbons
Good, and the elastomer usually becomes the limit before the metal does
Move the review to seal material choice
Steam and hot condensate
Good metallurgically
The elastomer and the thermal cycling, not the alloy, decide service life
Two lines in that table do most of the damage in real plants. Hydrochloric acid is not a grade selection problem at all, and hypochlorite is the one people get wrong because it looks like “just washdown water”. Both are covered, along with the 304 to 316 boundary, in our comparison of 304 versus 316 stainless steel cable glands.
The Three Crevices Inside a Gland
Stainless fails here by crevice corrosion far more often than by uniform attack, and a gland contains three crevices by design. The thread root where the body screws into the enclosure is an interrupted helical gap that holds liquid and excludes oxygen. The seal-to-bore interface is the second. Under the locknut and washer, where the contact face traps a thin film, is the third.
You cannot eliminate these. What you can do is stop them becoming permanent wet pockets: a drip loop in the cable before the entry, a downward-facing orientation, a drilled weep or a shroud where water can stand in the dome nut. Any of those is worth more than upgrading the alloy a step.
A related point often missed: the crevice does not need process chemical to start. Condensate that has picked up chloride from the atmosphere or from washdown is enough, which is why gland failures cluster on the north face of outdoor structures rather than on the process-wetted side.
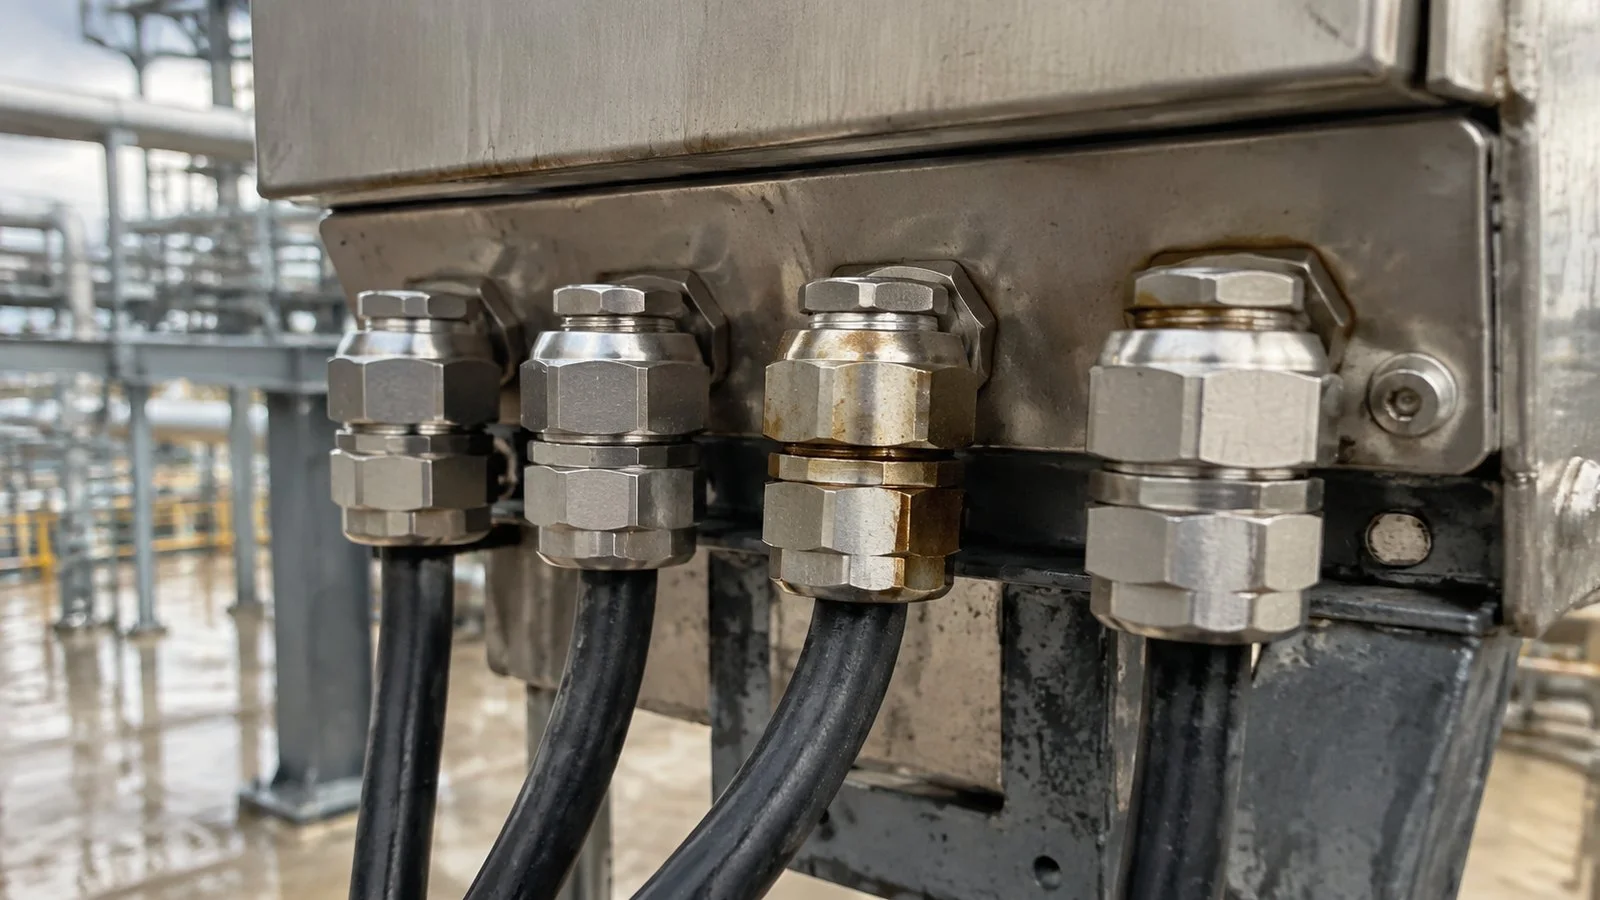
Stainless steel cable glands in service on an outdoor chemical plant enclosure. Discolouration appears at the thread and body long before any leak.
Behind a gland plate or on a ledge under an entry, product accumulates and never rinses; a crystallising salt holds moisture against the metal and re-wets on every humidity rise. Slope the plate, seal it to the enclosure, and drain the low point.
Welded Gland Plates: Heat Tint and Passivation
Most 316L gland failures blamed on the grade are actually fabrication defects. Welding burns off the passive chromium oxide layer and leaves a heat tint that is chemically different from the parent metal. That tint is where pitting begins, and if it sits on the wet side of a plate it will pit before the gland body shows anything.
The order of operations matters more than the chemical used: weld, mechanically remove heat tint and embedded iron, passivate, then install glands. Installing glands first means abrasive dust and iron particles end up inside the thread and under the washer.
Free iron is the quiet killer. Carbon steel wire wool, a worn grinding disc, a steel brush borrowed from another job, or a bench shared with mild steel all deposit iron onto 316L. The iron rusts, the rust holds chloride, and a pit opens under it. That is worth a dedicated stainless-only tool set, painted a different colour, and a rule that nobody signs out the wrong one.
CIP, SIP and Cleaning Chemicals
Cleaning chemistry is frequently the real service condition, not the process fluid. A gland that only ever sees a benign product can still be destroyed by the wash cycle it receives twice a day.
Cleaning agent
Effect on 316L
What to control
Dilute sodium hydroxide, hot
Generally acceptable
Temperature and concentration together; caustic cracking risk in stressed parts
Nitric acid passivation
Benign, and beneficial
Use it as scheduled maintenance after any mechanical damage
Sodium hypochlorite sanitiser
Aggressive; pitting and crevice attack
Minimise contact time, rinse thoroughly, never leave to dry in place
Chlorinated alkaline foam
Aggressive for the same reason
Verify the actual free chlorine level, not the product name
Phosphoric and nitric acid blends
Usually acceptable when controlled
Confirm the blend and temperature with the chemical supplier
Steam sterilisation
Metallurgically fine
Thermal cycling drives seal compression set long before the metal notices
Whatever the metal does, remember that the seal is on the same duty and is usually the first component to fail. Elastomer selection for these duties is set out in our guide to EPDM, NBR and silicone cable gland seals, and the two decisions should be made together, not sequentially.
Chlorides: The Variable That Decides Most Outcomes
If one variable governs the life of a stainless gland it is chloride concentration, and the second is temperature. They interact: an alloy comfortable in cold dilute chloride will pit in the same concentration hot. Because the interaction is continuous rather than a threshold, we do not publish a single maximum chloride figure, and anyone who does should be asked what temperature and crevice condition it assumes.
Practically, record the chloride level of every stream, washdown and condensate included, and treat the highest as the design case. A gland is an intermittent-wet component, so what matters is the concentration left behind when the water evaporates, which is higher than the bulk liquid.
A One-Page Spec for a Chemical Plant Gland
The fastest way to stop repeat failures is to make the requisition specific. A line that says “SS cable gland, M20” will be filled with whatever the distributor has, and the differences are exactly the ones that matter.
Field
What to write
Why it matters on site
Grade
316L, with the UNS or EN designation spelled out
“Stainless” alone permits 304, and 304 will fail where 316L survives
Material certificate
EN 10204 3.1, matched to the heat number
The only way to prove what was installed after the fact
Thread and size
Full designation including pitch, for example M20 x 1.5
Prevents a PG part being substituted where an M part is required
Cable range
The measured sheath diameter range, not the nominal cable size
A cable at the extreme of the range seals poorly from day one
Ingress protection
IP68 with the test depth and duration stated
“IP68” without conditions is not a specification
Seal material
Elastomer type named explicitly
The seal is usually the first failure, and it is invisible in a catalogue photo
Surface condition
Pickled and passivated, free of heat tint
Heat tint is a pitting site regardless of grade
Accessories
Locknut, washer and shroud in the same grade
A 304 locknut on a 316L body creates a galvanic couple at the wettest point
Our stainless steel cable gland range is supplied against this kind of line item, in metric and PG threads, with dimensional data published per size so the spec can be checked before ordering.
Installation Discipline That Protects the Alloy
The alloy only performs if the installation does not damage it. Use stainless or plastic tooling on the body, because a chrome vanadium spanner leaves a smear of less noble metal in the flats. Never use chloride-bearing anti-seize on the thread, and keep paint out of it. Do not mix grades inside one assembly: a small anode against a large cathode at a thread is the worst galvanic geometry there is.
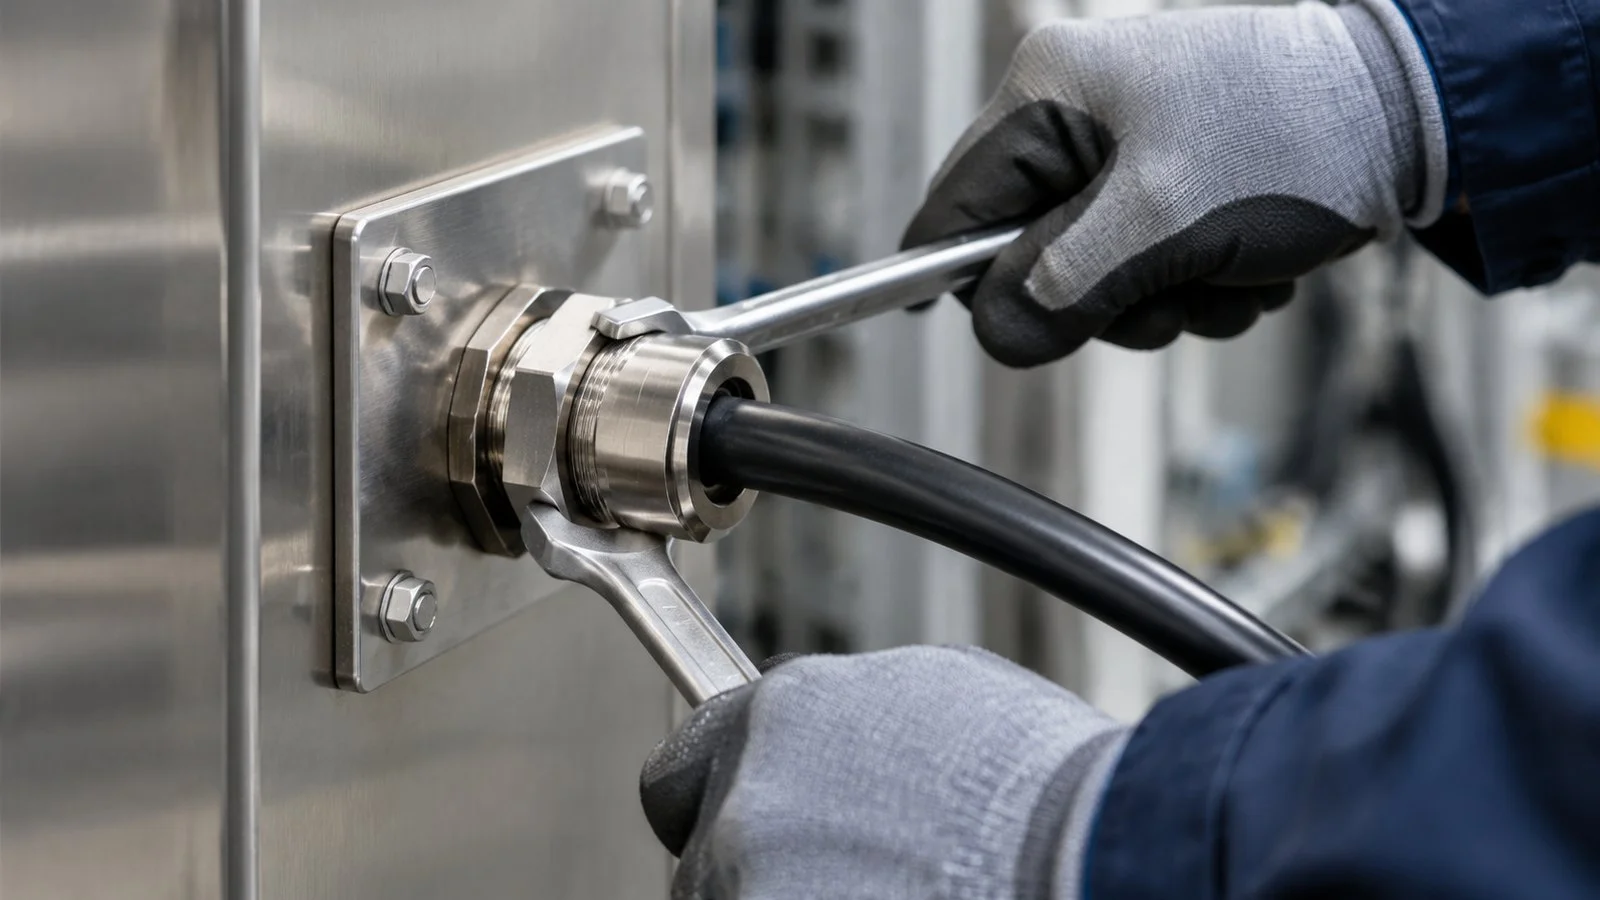
Two wrenches on a stainless gland: one holds the body, one turns the dome nut, so the torque goes into the seal and not into the panel thread.
Torque belongs to the gland design and the enclosure material, not to the alloy, so it comes from the datasheet of the part actually supplied. What site can check is the outcome: seal visibly compressed, body not bottomed out on the plate, no thread showing beyond the locknut. Our cable gland torque guide explains how to read a datasheet value and what to do when there is none.
Inspection and Replacement Triggers
Stainless gives warning, and it is visible if anyone looks. Tea staining is a stain rather than a failure, and can be removed and repassivated. Sharp-edged pits with a dark centre are a failure in progress and mean the environment has exceeded the grade. Rust bleeding from a thread root means free iron. A crystalline deposit at a seal means the gland is wet and drying repeatedly, which is a design fault, not a material one.
The routine is a walk-down twice a year on the entries carrying the highest chloride load, photographed from the same angle and filed against the tag number. A four-millimetre pit looks like nothing until you can see it was two millimetres last year, and that record is what makes the next alloy decision evidence-based.
Is 316L always better than 304 for a chemical plant?
For chloride-bearing and acidic duties, yes, and the molybdenum is the reason. For dry, sheltered indoor entries carrying benign media, 304 is adequate and the extra cost buys nothing, which is why a plant-wide blanket upgrade is usually wasted budget.
Can a stainless gland be used on a hydrochloric acid line?
No. Hydrochloric acid attacks austenitic stainless regardless of grade, and no practical alloy upgrade inside a gland budget changes that. The entry needs a non-metallic body or a fully isolated and lined arrangement.
Why did our 316L glands stain brown within a year?
Nearly always free iron contamination or retained heat tint from fabrication, not the alloy itself. Both are surface conditions, both can be removed, and both are preventable by cleaning and passivating the plate before glands are installed.
Do we need a material certificate for every gland?
Where a failure has safety or contamination consequences, yes, at least a 3.1 certificate traceable to the heat number. It is the only defence when a substitute grade is offered during a shortage.
Does a higher IP rating solve a chemical plant problem?
No. Ingress protection describes water entry under defined test conditions; it says nothing about chemical resistance or crevice corrosion on the outside. The two specifications answer different questions, and both need writing.
An explosion proof cable gland protects the one part of a flameproof enclosure that cannot be welded shut. How it works, why IP68 is not Ex, and the four compatibility checks that decide whether a correctly fitted gland is still the wrong one.
Brass cable glands for harsh industrial environments: the load combinations that break them, where brass beats stainless, what heavy duty really changes, and the upgrade order.
When it comes to ensuring the safety, durability, and efficiency of electrical installations, the humble Cable Gland plays a critical role. Whether you’re working in industrial automation, oil and gas, telecommunications, or renewable energy, choosing the right cable gland can make all the difference in the performance and longevity of your systems. In this article, we’ll explore […]
We use cookies to enhance your browsing experience, serve personalised ads or content, and analyse our traffic. By clicking "Accept All", you consent to our use of cookies.