An industrial cable gland in a fixed cabinet is judged by years. In an automation cell it is judged by cycles, and those cycles arrive far faster than most people expect: a cable carrier running a 600 mm stroke at one hertz accumulates two million cycles in three weeks of production. A gland that was specified for years of static service is being asked to survive that.
This is why automation failures cluster at the cable entry rather than anywhere else in the cabinet. The components inside are protected, derated and documented. The brass cable gland on the moving axis is usually the last thing anyone models, and it is the first thing to leak, loosen or cut a sheath.
The Three Loads a Moving Machine Puts on an Entry
Everything an automation environment does to a gland reduces to three loads. They fail differently, and a part that answers one often makes another worse.
Load
What it does to the gland
What actually answers it
Cyclic flex
Bends the sheath at the exit of the seal until it work-hardens and splits
Moving the flex point away from the gland with a support or clamp
Vibration
Backs the thread off and relaxes the elastomer preload
Positive locking on the thread, and a seal that resists compression set
Washdown and chemistry
Attacks the seal compound first, then the plating or the polyamide
The trap is that tightening the gland is the instinctive response to the second load, and over-tightening accelerates the first. A compressed seal that has been squeezed past its working range will grip the sheath harder at the exit point, which turns a gradual bend into a crease, which is where the split starts.
Cable Carriers and Moving Axes: When a Gland Is the Wrong Part
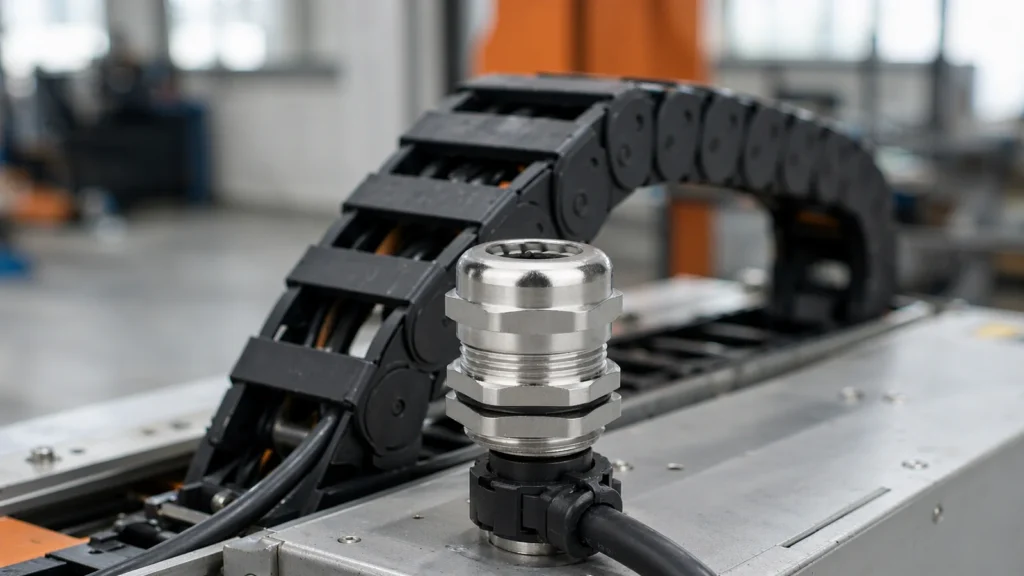
A gland belongs at the point where a cable enters a fixed enclosure. It does not belong at the moving end of a carrier, and it does not belong anywhere the cable is expected to flex repeatedly. In those places, a gland is a hard clamp at the worst possible location.
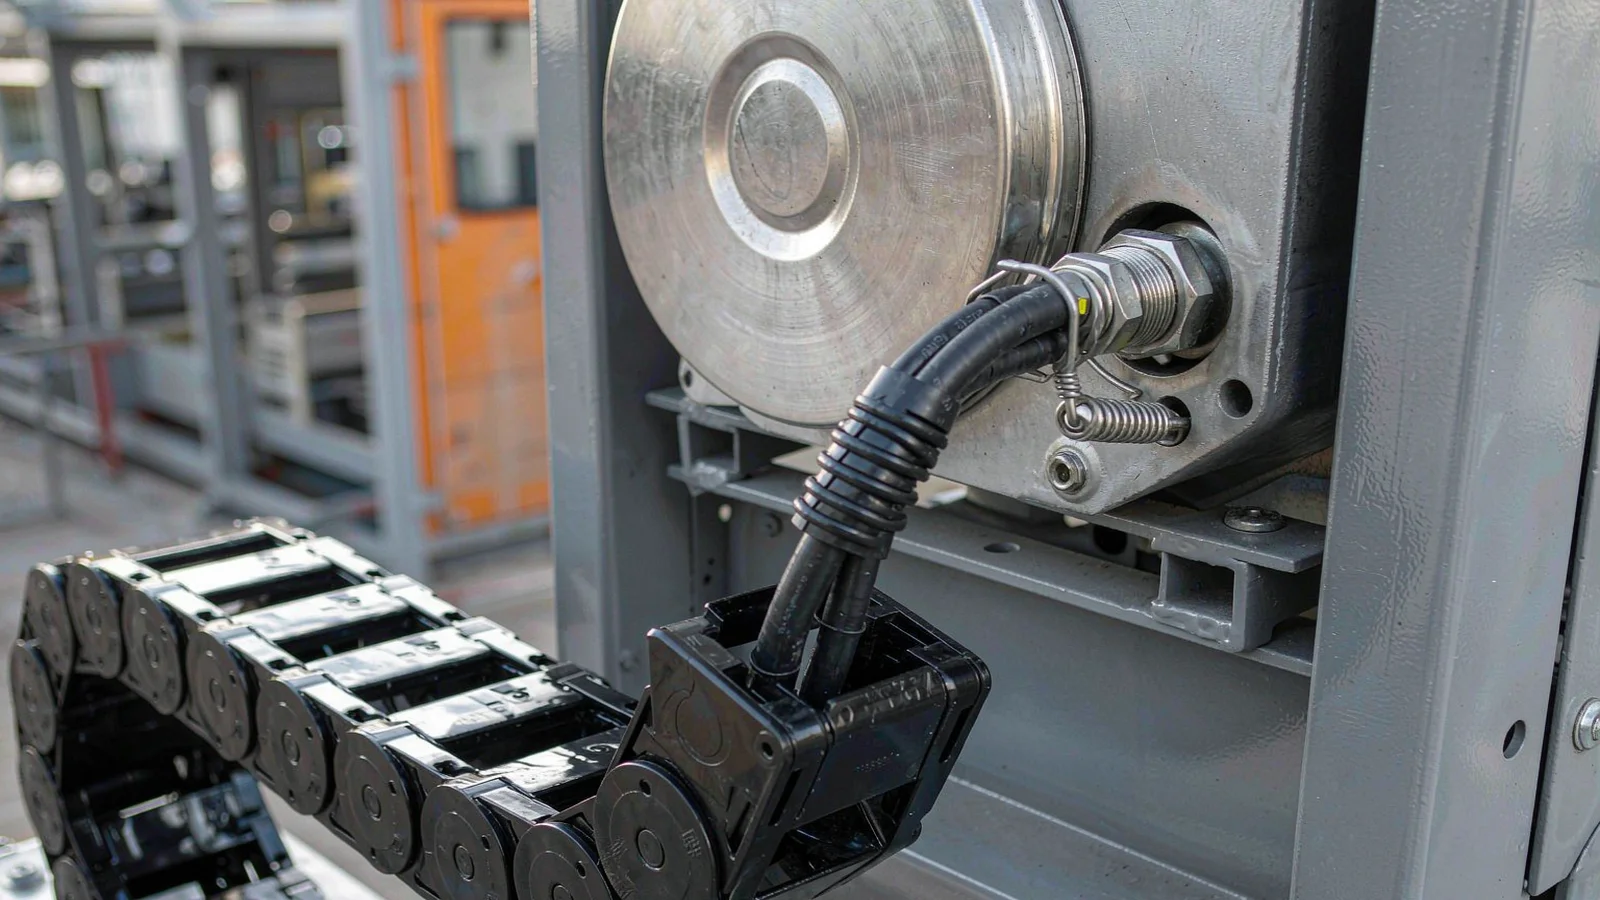
The pattern that works: gland at the cabinet, then a proper strain-relief clamp on the carrier, then the cable dressed with the radius its datasheet demands along the whole travel. The gland’s only job is to seal the cabinet and stop pull reaching the terminals. The carrier’s job is to absorb the motion, and it needs a clamp that grips the sheath over a length rather than compressing a ring.
Where the cable must flex close to the enclosure — a short-travel gantry, a pendant on a boom — the fix is distance, not a better gland. A bracket that stands the entry off the wall by 100 mm buys more service life than any sealing upgrade, because it moves the flex point out of the seal. Where a panel is being retrofitted and the cable cannot be re-terminated, a split cable gland avoids cutting the connector off, but it is a retrofit answer, not a motion answer.
Gland at the enclosure, clamp on the carrier. The gland seals; it should never be the part that absorbs the motion.
Vibration: What Actually Loosens a Gland
A gland does not come loose because the machine shakes it. It comes loose because vibration lets the joint relax in small increments, and two mechanisms do the relaxing.
The first is thread back-off. Under transverse vibration, mating threads slide against each other a few micrometres at a time and the preload walks away. The second is elastomer creep: the seal and any nylon component lose preload gradually, so a joint that was correct on installation becomes under-torqued without anyone touching it.
Metal parts resist the second mechanism, not the first. Nickel-plated brass holds preload; polyamide creeps. On a vibrating machine, that alone decides the material.
Lock the thread positively. A locknut bearing on the wall, a serrated washer, or a thread-locking compound applied as the manufacturer allows. The exact choice matters less than the fact that it was decided.
Re-torque on a schedule tied to the machine, not the calendar. After the first week of production, again after the first thermal cycle, then at planned maintenance. A torque value written on a drawing is only useful if someone checks it once (see the torque guide).
Washdown Cells: IP69K, Materials and the Traps
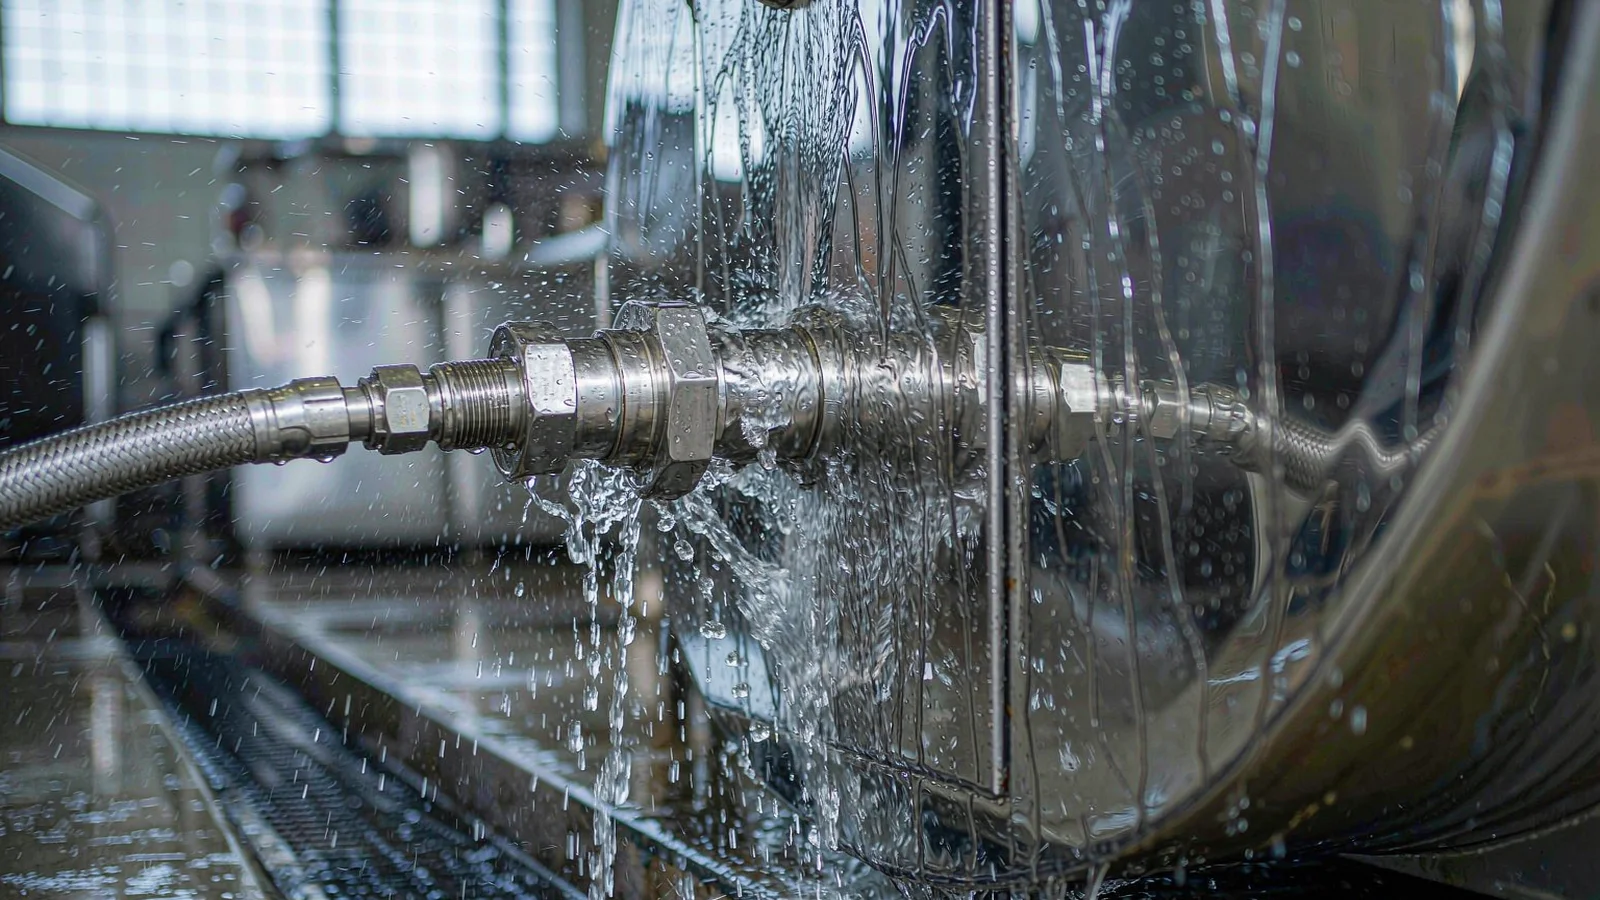
Food, beverage and pharmaceutical cells combine water at pressure with cleaning chemistry, and the two together are harder on a gland than either alone.
IP69K describes resistance to a high-pressure, high-temperature jet at a defined distance and angle. It says nothing about chemistry. A gland can pass the jet test and still fail in six months because the caustic wash has hardened an NBR seal into a brittle ring, or because the chlorinated rinse has pitted the plating on a brass body.
Exposure
Risk to the entry
Practical direction
High-pressure hot water
Jet drives past a seal that is not fully compressed; steam reaches the insert
Correct jet angle, thread sealant per maker, verified seal compression
Alkaline and acid wash cycles
Elastomer hardens and cracks; alternate chemistry stresses both
Confirm the compound against the actual cleaning agents, not against water
Chlorinated rinse
Plating pitting on brass; stainless stains but survives
Stainless housing with a compatible seal
Product dust and sugar
Builds up behind the locknut, holds moisture
Stand-off entry, smooth surfaces, access for cleaning
Ask the cleaning contractor for the chemical list before choosing a seal. It is a two-line email that prevents most washdown failures.
Robot and Gantry Enclosures: Mass, Radius and Access
On a robot or a gantry, the enclosure is often small, mounted high, and carries cables that are heavier than the cabinet designer assumed. Three constraints follow.
Mass matters because every gram of cable hanging off an arm becomes a load on the arm and a pull on the entry. Support the cable with a bracket at the enclosure so the gland never carries weight. Radius matters because a compact enclosure gives the cable very little room to turn after the seal, which is the same failure described above with less space to solve it. Access matters because a gland mounted on the underside of a box at head height will be inspected once and then forgotten — put it where a technician can reach it with a wrench.
Sensor Cables: Gland or M8/M12 Connector?
Not every entry in an automation cell should be a gland. The dividing question is whether the cable will be disconnected in service.
Permanent, protected, terminated once: gland. Cheaper per point, better sealing, no mating interface to corrode.
Disconnected for cleaning, changeover or tooling swap: connector. A gland that is opened twice a week will be destroyed by the third week.
Very small cables and very high density: multi-entry insert or a connector block, because thirty M12 cables through thirty glands will not fit on the plate.
The junction between the two is where mistakes live: a sensor cable glanded into the cabinet and an extension lead with a connector hanging in a wash zone. Either protect the connector or move the joint inside.
Drive and Encoder Cables: Two Different Shielding Jobs
Both cables are screened and both are often specified with the same gland, which is where the trouble starts. The screens are doing different work.
A motor cable screen carries the drive’s common-mode current back to the drive. It needs a low-impedance bond at both ends and a circumferential contact at the enclosure entry — a drain wire taken to a terminal does not do this job. An encoder or analogue signal cable screen is protecting a small signal from a large field; the bond is still best at the entry, but the cable’s own construction and the symmetry of the pair do most of the work.
If a drive is tripping on overcurrent or an encoder is counting noise, the entry is the first place to look, and a partially-dressed screen is the usual finding. The VFD cable gland article covers the motor side in detail; the shortcut for specifying is that the gland must give circumferential contact, not a single wire.
A jet is a mechanical load, not a chemical one. Passing the spray test says nothing about the cleaning agents.
Retrofit and Export: Documentation for the Next Engineer
Automation equipment travels. A cell built in one country is installed in another, maintained by a third party who has never seen the drawing, and modified on site with whatever the local distributor stocks.
Three records prevent the worst outcomes: the gland schedule with cable diameters and thread types, a photograph of the entry plate as built, and a note of the seal compound used per entry group. Without them, the first field replacement will be chosen by thread size alone, and the machine will come back with a leak that nobody can explain.
Where a machine ships to a market with a different thread convention, decide now whether to fit adaptors at the factory or supply a spare gland kit in the local thread. Adaptors add a joint, a length and a bonding interface; a kit costs freight and keeps the installation single-piece.
The Automation BOM
Four lines cover most cells. Build them by where the cable goes, not by cable diameter.
Location
Requirement
Typical choice
Fixed cabinet, indoor
Grip, seal, low cost at volume
Nickel-plated brass, standard insert
Moving axis or carrier end
No flex at the seal; support by clamp
Gland plus bracket stand-off and carrier clamp
Washdown or food zone
Jet resistance plus chemical compatibility
Stainless housing, seal matched to the cleaning agents
Serviced sensor point
Repeated connect and disconnect
M8/M12 connector, not a gland
How often should glands be re-torqued on a vibrating machine?
At the first scheduled maintenance after commissioning, then at each planned stop. Checking by calendar rather than by machine hours is guesswork.
Will a nylon gland survive a washdown cell?
Only if the cleaning agents are compatible and the temperature stays inside the material’s range. Alkaline and chlorinated cycles are the usual reason polyamide entries crack.
Can I use a standard gland on a robot arm?
As a seal at the enclosure, yes, provided the cable is supported and the flex point is moved away from the gland. It will not survive being the flexing element itself.
Why do drive cables need a different gland from sensor cables?
The screen on a motor cable carries the drive’s common-mode return current, so it needs a low-impedance circumferential bond at both ends. A single drain wire raises that impedance by orders of magnitude.
What is the most common cause of a leaking entry on a moving machine?
A sheath that has been creased at the seal by too tight a bend immediately behind the gland. The leak is a symptom; the cause is the routing.
Send the axis layout, cable list and cleaning agents, and we will flag which entries need a stand-off bracket, which need a washdown-grade seal, and where a connector would be cheaper than a gland over the life of the cell. Start from the strain relief guide for the mechanical side, or the stainless range for washdown and food zones.
Brass and stainless steel cable glands compared size for size: weight, conductivity, temperature, galling, chloride failure mode, galvanic coupling and what the price gap actually buys.
A leaking cable gland is rarely a faulty gland. Read the water to find which of the four entry routes it used, match the symptom to the interface that failed, and fix the cause instead of replacing the part again.
We use cookies to enhance your browsing experience, serve personalised ads or content, and analyse our traffic. By clicking "Accept All", you consent to our use of cookies.