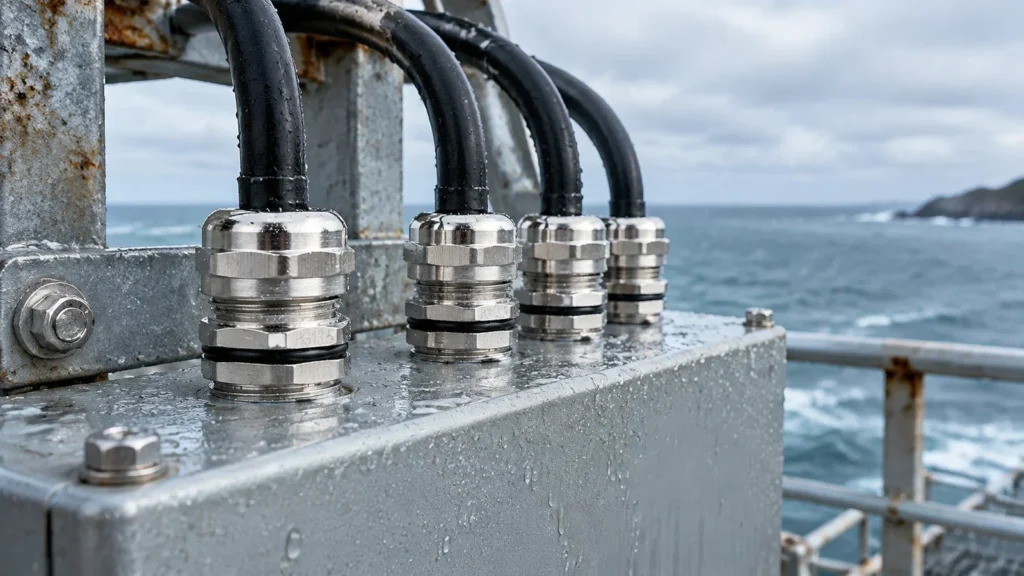
Ask five suppliers for a corrosion-resistant cable gland and you will get five different claims: “salt spray tested”, “marine grade”, “corrosion resistant to 500 hours”, “passivated”, “suitable for coastal sites”. None of those phrases is wrong, and none of them is a specification. They describe test methods, surface treatments and marketing positions, and a buyer cannot rank them without knowing what each one actually measures.
This page is about reading the evidence. It is not a grade comparison and not a material primer; those are covered elsewhere. It is about the gap between a claim on a datasheet and a gland that is still intact after four years on a jetty.
Corrosion Resistance Is Not a Single Number
Corrosion is a family of mechanisms, and a material can be excellent against one while failing badly at another. Uniform attack thins a surface evenly and is comparatively honest. Pitting concentrates on a tiny area and perforates long before any loss is visible. Crevice corrosion needs a geometry, not a chemical, and stress corrosion cracking needs a tensile stress plus a specific environment. Galvanic attack needs two metals and an electrolyte.
A gland in service can experience all five, which is why a single number cannot describe performance, only one test under one set of conditions.
What a Salt Spray Test Actually Proves
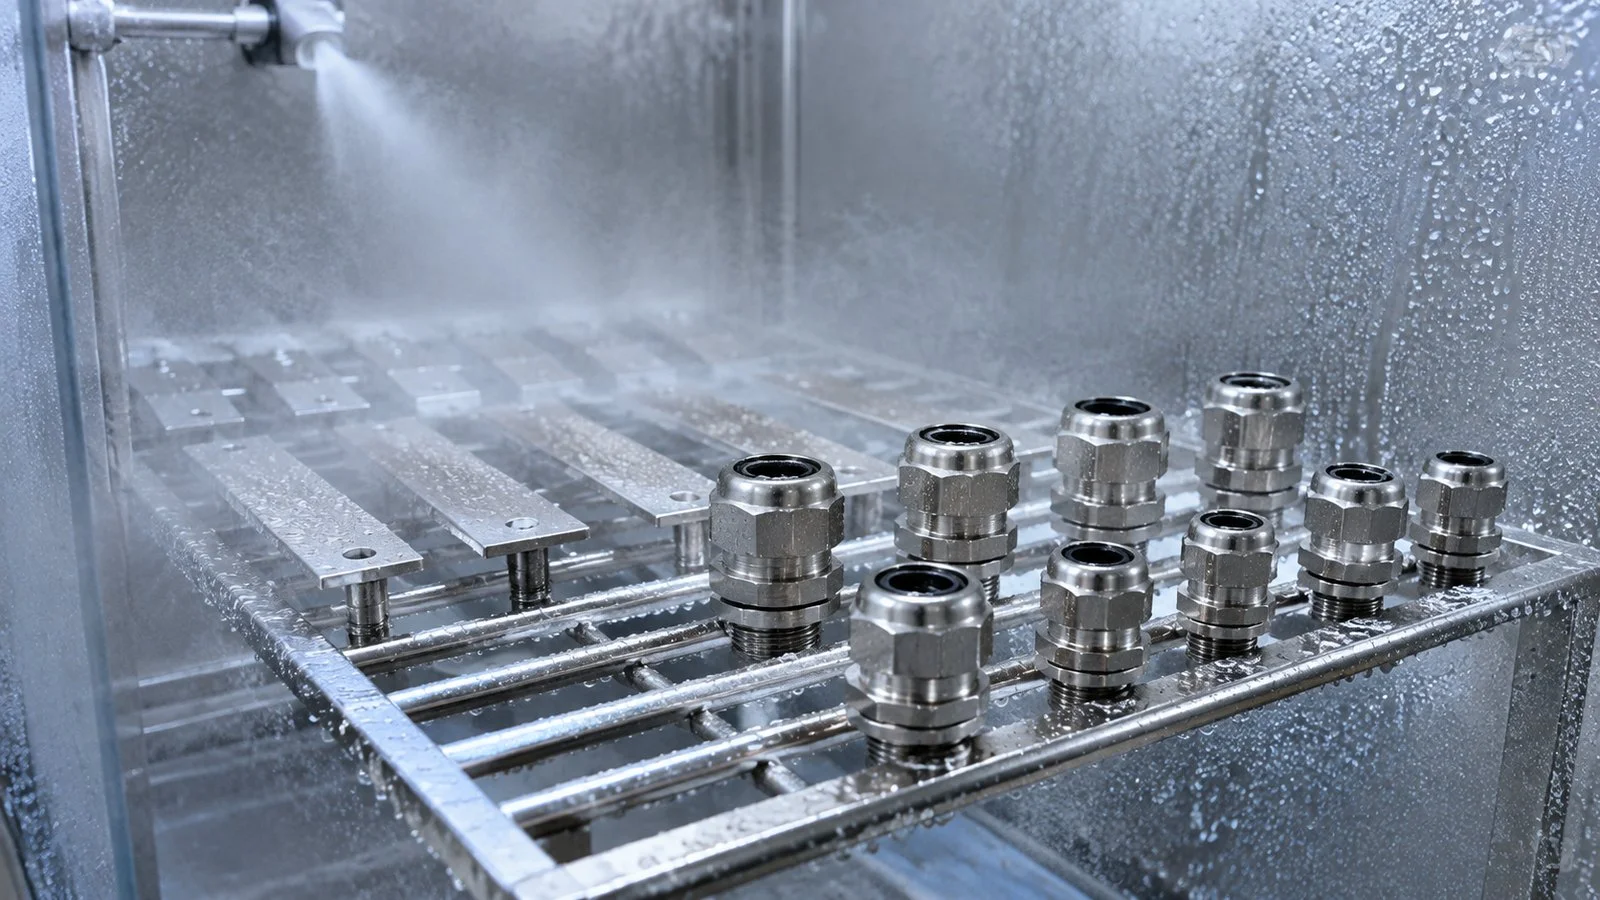
Neutral salt spray, the fog test defined in ISO 9227 and ASTM B117, is a quality-control screening test. It exists to detect a difference between two nominally identical production batches, and it does that job well. It is not a service-life prediction, and the hours figure has no general conversion into years.
The reasons are structural. The test runs a continuous fog at a fixed temperature with no drying cycle, no UV, no sulphur compounds and no crevices unless the sample happens to have some. A coastal installation cycles wet and dry daily, concentrates chloride as it dries and holds the residue in thread roots, which is close to the opposite condition.
There is a second problem specific to stainless. Austenitic stainless protects itself with a passive chromium oxide film, so under salt fog it fails by pitting and crevice attack at a defect rather than by gradual wastage. The result therefore depends heavily on surface condition. A passivated 316L sample and a heat-tinted 316L sample of the same heat can differ by an order of magnitude in time to first pit, so two suppliers’ hours are comparable only if preparation, geometry and acceptance criterion all match.
Gland samples on a rack inside a neutral salt spray chamber. The test produces a comparable number, not a service life.
Test
What it measures
What it cannot tell you
Neutral salt spray, ISO 9227 NSS
Relative resistance to chloride fog under fixed conditions
Service life, or performance under wet-dry cycling and UV
Acetic acid salt spray, AASS
Faster screening, more aggressive than NSS
Anything about acidic process media
Copper accelerated salt spray, CASS
Decorative and plated finishes, very aggressive
Bare stainless performance, which it distorts
Immersion or cyclic immersion
Behaviour in a defined liquid at a defined temperature
Atmospheric and crevice effects, unless crevices are built in
Ferroxyl or ferricyanide test
Free iron contamination on the surface
Anything about alloy choice or general resistance
Three Factors You Can Actually Control
Since the test does not predict life, the practical approach is to control the three factors that do, and to buy accordingly. They are alloy, surface and geometry, and in our experience of field failures they rank in exactly that order of how often they are specified, and the reverse order of how often they are the cause.
Alloy is the part everyone argues about and usually the part that is already adequate, since a 316L body suits most coastal and washdown duties. If the site is genuinely aggressive, the next step is not “more stainless” but a grade with a higher pitting resistance equivalent, or a non-metallic body. Our comparison of 304 and 316 stainless steel cable glands covers that boundary.
Surface is the part that is usually skipped. A passivated surface with no heat tint and no embedded iron performs very differently from the same alloy left as-welded or ground with a contaminated disc. This single factor explains most of the “identical glands, different outcomes” cases on the same structure.
Geometry is the part nobody owns. If the design puts a horizontal entry where water stands, or leaves a flat ledge under a gland plate, the best alloy on the market will fail there while a 304 gland two metres away on a downward entry is fine. Geometry beats material every time a pocket is involved, which is the central argument in our guide to 316 stainless steel cable glands in marine service.
Reading the Pitting Resistance Equivalent
When a claim needs to be compared numerically, the honest metric available to a buyer is the pitting resistance equivalent number, calculated as chromium plus three point three times molybdenum plus sixteen times nitrogen. It captures the three elements that drive pitting resistance and nothing else.
On that scale 304 sits in the high teens, 316L in the mid twenties, and the super-austenitic and duplex families in the mid thirties. The number is useful for comparing alloys. It is not a service limit, because it contains no term for temperature, chloride concentration, crevice geometry or surface finish. Two sites can have the same PREN requirement and completely different outcomes.
Asking for Evidence Instead of Adjectives
The way to convert a marketing claim into a purchase condition is to specify the report, not the adjective. A supplier who has genuine data will produce it without argument, and the ones who cannot will negotiate on price instead, which is itself useful information.
What the supplier says
What it really means
What to ask for
“Salt spray tested”
A test was run; conditions and criterion unstated
Standard, sample preparation, hours and the acceptance criterion used
“Marine grade”
No defined meaning in any standard
The actual alloy designation and surface treatment
“Corrosion resistant”
Nothing measurable
A grade, a PREN value and a passivation statement
“Stainless steel”
May be 304, 316, 316L or a casting grade
Exact designation plus a 3.1 material certificate
“Passivated”
Usually true and usually undocumented
Method used, and whether heat tint was removed first
“Tested to IP68”
Water ingress, not corrosion
Depth and duration; it says nothing about chemical duty
Recognising the Failure Mode On Site
Once a gland is in service, the appearance of the damage identifies the mechanism, and the mechanism tells you which of the three factors was wrong. This is the most under-used diagnostic in maintenance, because most reports simply say “corroded” and replace the part without learning anything.
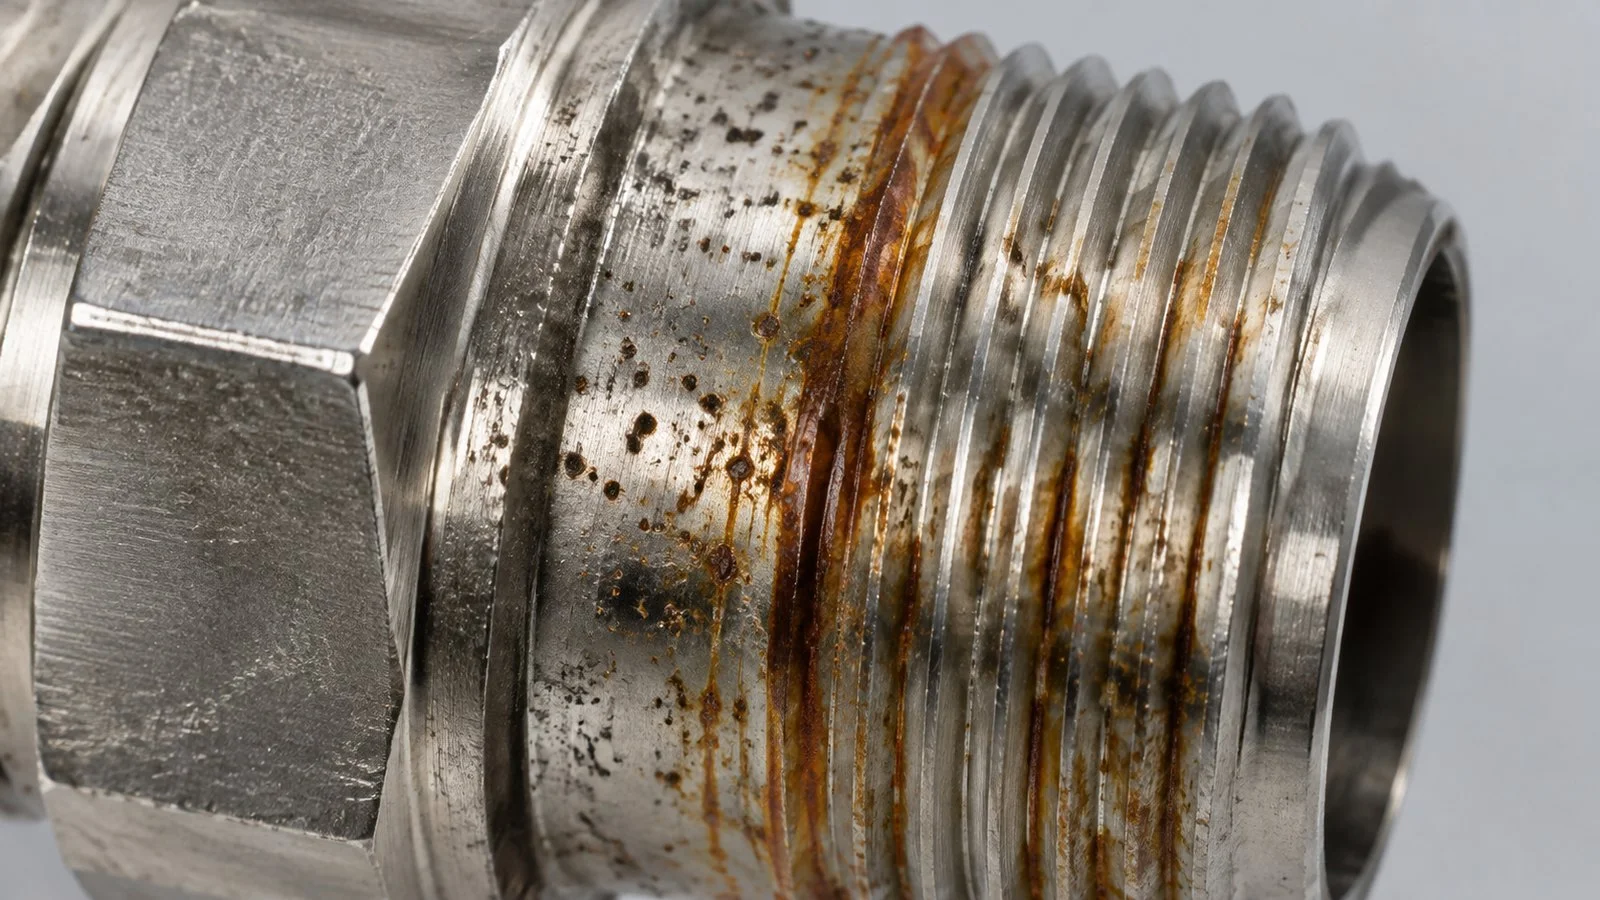
Pits with dark centres and rust streaks running from the thread root: the pattern that tells you which of the three factors was wrong.
What you see
Most likely mechanism
Correct response
Uniform light brown film, no pitting
Tea staining, surface contamination
Clean and repassivate; no material change needed
Rust streaks running down from a thread or a weld
Free iron contamination
Fix the fabrication process, not the alloy
Sharp pits with dark centres, scattered
Chloride pitting, environment above grade
Re-grade, or reduce chloride exposure
Attack confined to a gap or under a washer
Crevice corrosion
Remove the crevice or drain it; dressing alone will not help
Roughened surface next to a dissimilar metal
Galvanic attack, usually a steel or zinc neighbour
Isolate the couple or match the grade
Cracks near a thread root, no metal loss
Stress corrosion cracking
Review stress, temperature and chloride together
Field Checks a Maintenance Team Can Run
Three checks need no laboratory. The water break test is the simplest: a clean, properly passivated surface holds a continuous water film for about thirty seconds, while a contaminated or organically soiled surface breaks into droplets immediately. It costs nothing and it catches a bad batch before installation.
A ferricyanide spot test detects free iron in seconds and is the only practical way to confirm that a gland plate was cleaned properly before assembly. A blue stain indicates contamination that will become a rust bloom within months.
The third is a photographic record: the same gland, the same angle, twice a year, filed against the tag. Progression is the diagnostic. A single photo of a stained gland tells you nothing; two photos a year apart tell you whether it is stable or moving.
Coastal, Washdown and Process Are Three Different Duties
Buyers often use one corrosion specification across a whole site and then wonder why it holds in one area and fails in another. The three common duties are not variations of one problem. A coastal site delivers airborne chloride and long wet-dry cycling with no chemical load at all. A washdown area delivers hot water, detergent and mechanical impact, usually daily. A process area delivers a specific chemical at a specific concentration and temperature, continuously.
Each one stresses a different part of the assembly. Coastal duty attacks surfaces and crevices. Washdown attacks seals and impingement points. Process duty attacks the alloy itself. A gland that is excellent on one is not automatically acceptable on the others.
Where Stainless Is the Wrong Answer
Buyers sometimes move to stainless to close a corrosion problem and find it does not help. That happens in three situations: a crevice geometry that would fail any austenitic grade, a chemical family that attacks stainless outright such as hydrochloric acid or hypochlorite, and a galvanic couple where the stainless becomes the cathode and accelerates the corrosion of its neighbour. In each case the fix is a design or chemistry change, and a more expensive alloy simply moves the failure.
If the duty is genuinely chemical rather than atmospheric, the deployment detail that matters is different from anything on this page. Our guide to 316L cable glands in chemical plants covers media boundaries, crevices inside the gland and the passivation sequence, and it is the right next read for process plant rather than coastal or washdown work.
For plated brass on the same duties, the coating rather than the substrate sets the limit, which is why the hours figure on a nickel-plated part means something different from the same figure on a stainless one. Our nickel plated brass cable gland guide explains how to read those numbers, and our stainless steel cable gland range lists the sizes with their thread and cable-range data so a grade decision can be checked against the actual part.
الأسئلة المتداولة
Does a higher salt spray rating always mean better corrosion resistance?
No. It means a longer time to a defined failure under one fixed test. Surface preparation and sample geometry affect that number more than alloy choice does, so two ratings are only comparable when everything else matches.
Is 500 hours of salt spray equivalent to five years outdoors?
No such conversion exists. The test has no drying cycle, no UV and no crevices, while a real site has all three. Hours are a screening figure for batch consistency, not a service-life estimate.
Can we compare a plated brass gland with a stainless gland using salt spray hours?
Not directly. Plated brass fails by coating breakdown and substrate exposure; stainless fails by localised pitting at a surface defect. The mechanisms are different, so the same hour count describes different things.
What is the single most effective corrosion upgrade?
For most failed installations it is removing the water trap, not changing the alloy. A downward entry, a drip loop and a drainage path fix more failures than a step up in grade, and they cost less.
Do we need to test every batch?
For critical entries, yes for free iron at least, since that check takes seconds and catches the most common fabrication fault. Full salt spray belongs in supplier qualification, not in every delivery.
A brass-first thread guide for cable glands: metric, PG, NPT and G availability, size and hole data, cut versus rolled threads, sealing points, and thread damage that cannot be repaired.
Strain relief keeps load off the terminals, not off the cable. The three mechanisms, what determines pull-out resistance, and when a gland is not enough.
M20 is the most mis-ordered cable gland thread in the world. This guide gives the published dimensions, the 20 to 20.2 mm hole, the 6 to 12 mm cable range and the thread length arithmetic, then compares M20 with M22, M25 and PG13.5.
نحن نستخدم ملفات تعريف الارتباط لتحسين تجربة التصفح الخاصة بك، وعرض إعلانات أو محتوى مخصص، وتحليل حركة المرور لدينا. بالنقر على "قبول الكل"، فإنك توافق على استخدامنا لملفات تعريف الارتباط.