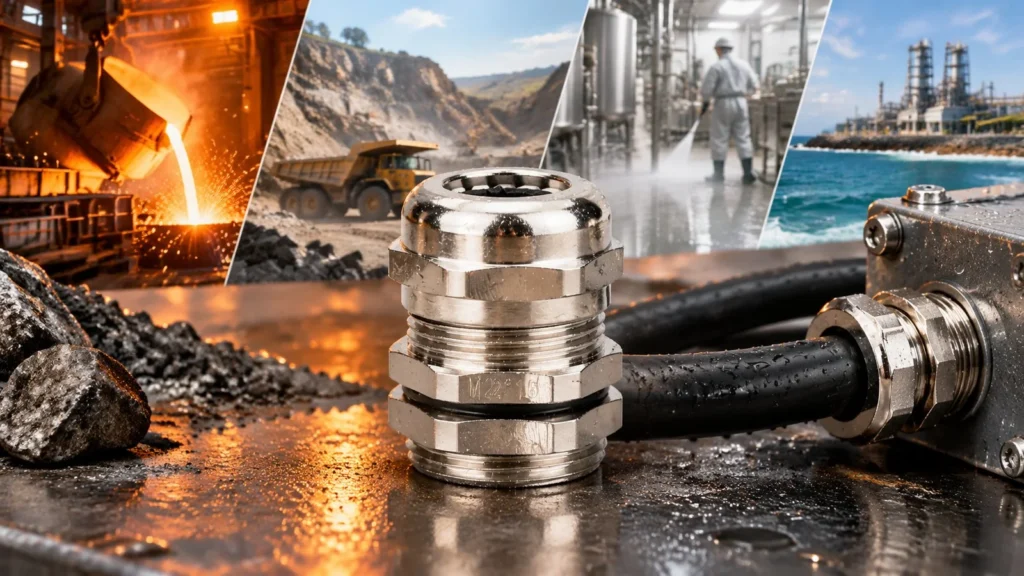
Every industrial site calls itself harsh. A clean machine shop with coolant mist and a foundry with radiant heat, mill scale dust and constant vibration are not the same problem, and a brass cable gland that lasts twenty years in the first may last eighteen months in the second.
This guide treats harsh duty as a combination of loads rather than an industry label. It covers which combinations break brass, what heavy-duty brass construction actually changes, the order in which upgrades are worth paying for, and when brass is simply the wrong material.
“Harsh” is a combination of loads, not an industry label
Six loads matter to a cable gland: heat, abrasion, vibration, chemical attack, UV and mechanical abuse. Brass handles any single one reasonably well. What destroys it is two or three arriving together, because the first one removes the protection that would have survived the second.
The pattern is consistent. Heat hardens the seal, then abrasion removes the surface that was protecting the body. Vibration loosens the joint, then chemical attack reaches the thread that was previously shielded. Salt removes the nickel, then the exposed brass dezincifies.
So the first question for any “harsh” enquiry is not which material, it is which two loads are present at the same time. The rest of this guide is organised around that.
What actually kills a brass gland in each setting
Setting
Loads present together
First failure
Verdict for standard brass
Steel mill, foundry, casting
Radiant heat plus mill scale dust plus vibration
Seal hardens and loses compression; then scale abrades the dome nut flats
Works only with a heat-rated seal and a shroud; heavy-duty body worth it
Cement, quarry, mining
Fine abrasive dust plus vibration plus washdown
Dust packs into the seal seat; vibration walks the dome nut back
Needs a separate clamping arrangement and frequent inspection
Food and beverage
Caustic CIP plus chlorinated sanitiser plus thermal cycling
Dezincification at the thread root; seal swell or hardening
Plated brass works in dry areas; washdown zones usually want stainless
Plating, pickling, acid stores
Acid mist plus condensate plus stagnant droplets
Nickel layer consumed locally, then brass attacked at the same spot
Not suitable; move to stainless or relocate the entry
Ports, marinas, coastal plant
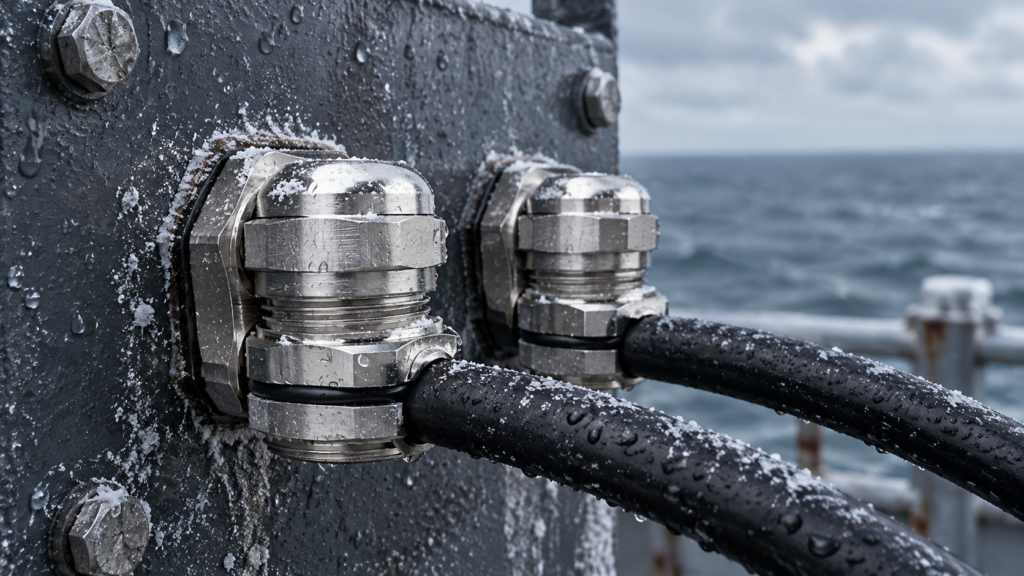
Chloride plus UV plus wind-driven spray
Coating loss on the dome nut, then white rust and thread stiffness
Plated brass with shroud is the minimum; stainless for structural entries
General factory floor
Oil mist, coolant, occasional impact
Physical damage from handling, not corrosion
Standard brass is the correct answer
The last row matters as much as the others. A large share of “harsh environment” specifications are written for a factory floor where standard brass with nickel plating will outlast the machine it is fitted to. Paying for stainless in that application buys nothing.
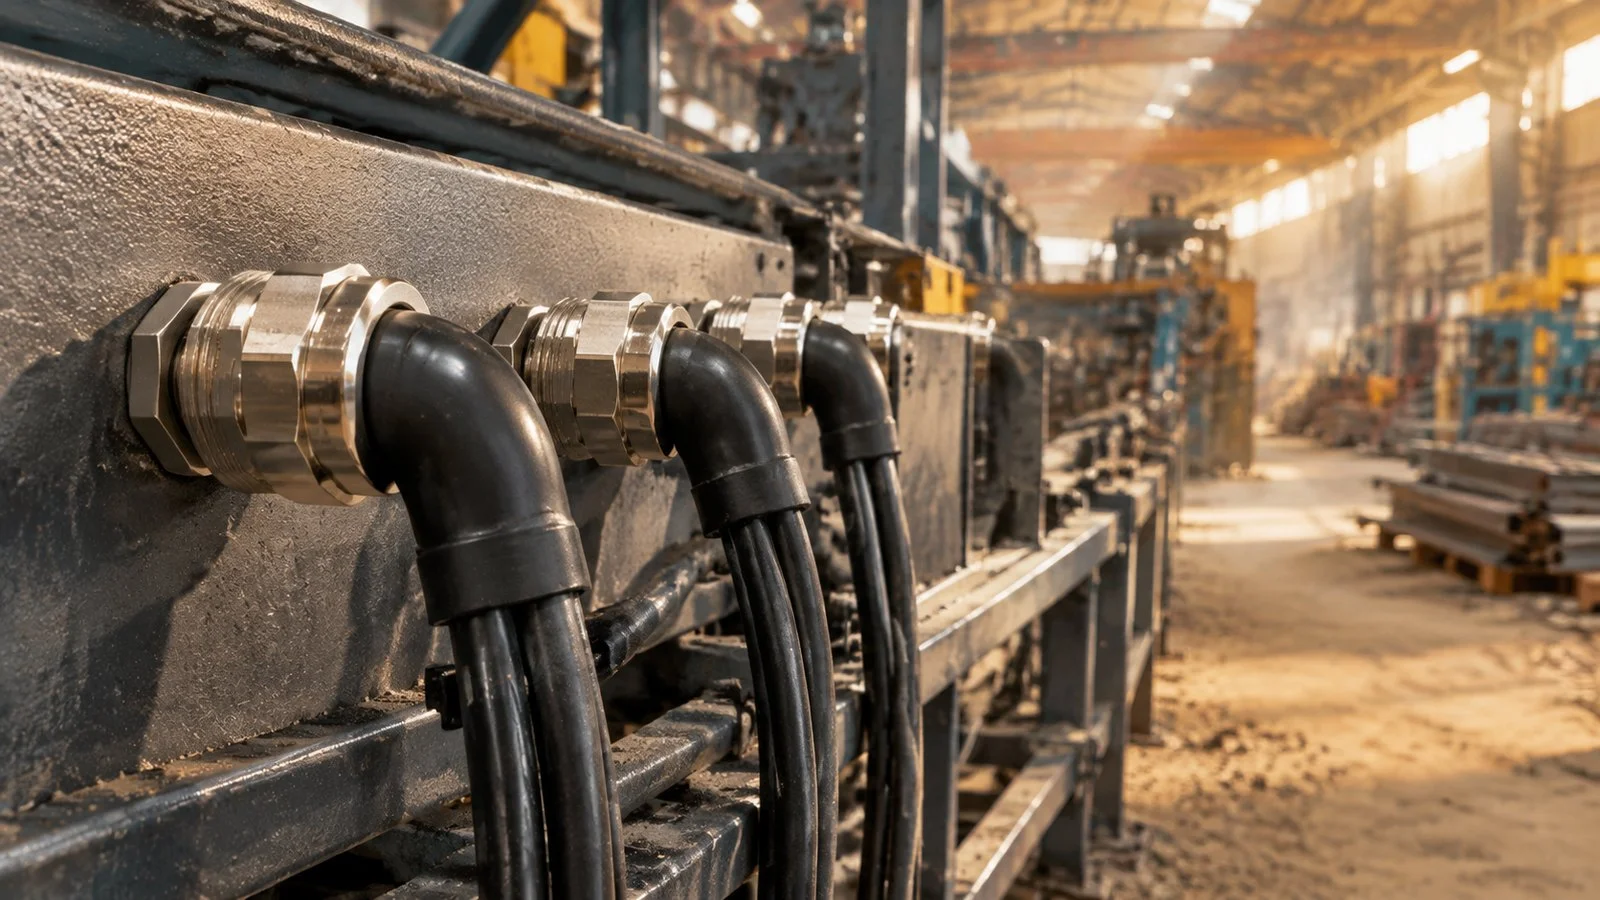
Nickel-plated brass glands installed on a steel fabrication line, with shrouds fitted over the bodies. The shroud takes the abrasion and weather so the plated thread underneath survives.
Where brass outperforms stainless in harsh duty
Stainless is the reflex answer for harsh environments and sometimes the wrong one. The material comparison in brass vs stainless steel cable glands sets out the trade-offs; four of them matter specifically here.
No galling. Stainless threads can seize into stainless entries, and the usual remedy on site is a saw. Brass threads do not gall in normal service, which matters on equipment that is opened for maintenance.
Thermal conductivity. Brass conducts heat away from the seal far better than stainless. Next to a hot surface that helps; on a hot enclosure it makes the gland a better heat path, so position matters either way.
Machinability. Brass takes a cleaner thread at lower cost, and thread quality is what seals and what resists stripping.
Cost and lead time. The gap is a multiple, not a percentage, and it decides whether a project can afford to fit plated brass everywhere or stainless only where it is needed.
Brass also fails visibly. Dezincification and white rust announce themselves months before the gland stops sealing, while a stainless entry can pit through without warning — a difference that changes how you inspect, not just what you buy.
What “heavy duty” means in brass, and what it does not mean
الميزة
Standard brass
Heavy-duty brass
What it buys
Body wall
Thinner section, adequate for hand tightening
Thicker section and larger hex flats
Survives impact and repeated re-tightening without deforming
Clamping
Single seal compresses on the sheath
Separate clamping ring, seal acts on its own
Grip and seal can be adjusted independently
Thread length
Standard GL
Longer thread option
Works on thick walls and through gland plates
Surface
Bare or thin plating
Nickel plating as standard, shroud supplied
Corrosion resistance from day one, not as an add-on
Armour handling
Not applicable
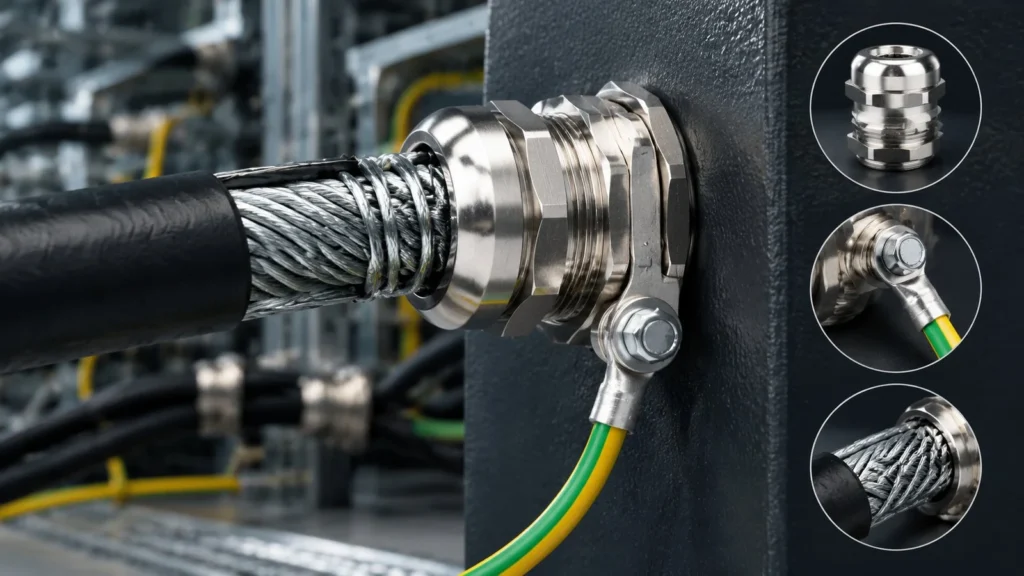
Armour cone and clamping ring included
Terminates SWA and STA without a separate kit
What it does not mean: a heavy-duty body does not improve the seal, does not raise the temperature limit, and does not make the gland suitable for a chemical it was not compatible with. Those are seal and material questions, not construction questions. A thicker body with the wrong elastomer fails exactly like a thin one.
The upgrade ladder: what to pay for, in what order
When a site is genuinely harsh, spend in this order. Each step addresses a different failure and the cheap ones come first.
Shroud. Cheapest upgrade and the highest return in abrasive or coastal settings. It takes the wear and the weather, and it protects the plated thread that does the sealing.
Nickel plating. Raises time-to-first-corrosion in chloride environments from months to years. What plating does and does not do is set out in the nickel-plated brass guide.
Heavy-duty body with separate clamping. Buys mechanical survival and independent grip adjustment, which is what vibration and washdown actually need.
Seal material change. Often skipped and often the real fix. EPDM, NBR and silicone fail for different reasons in different media; the differences are covered in seal materials.
Material change to stainless. Last, because it costs the most and still needs the right seal. Where the driver is heat rather than corrosion, the constraint is the seal chain, not the body — see high temperature cable glands.
Most “brass failed in a harsh environment” cases resolve at step one, two or four. Skipping to step five is the expensive way to discover that the seal was wrong.
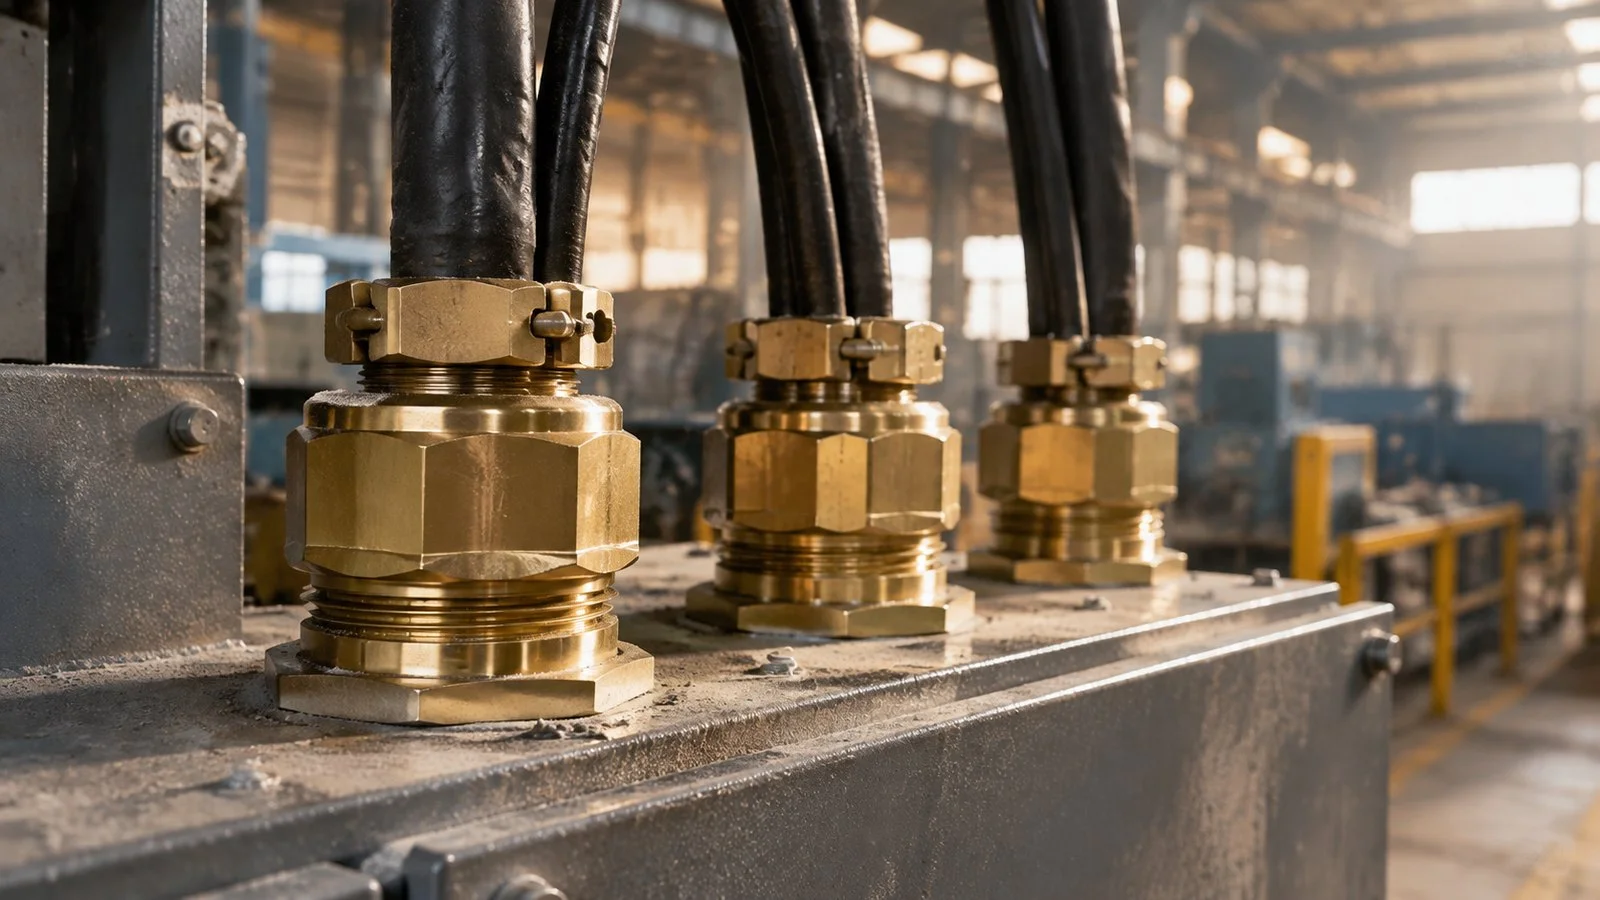
Heavy-duty plated brass glands on a machine frame in a dusty production hall, with the larger hex bodies and separate clamping nuts visible.
Seals are the short-life part in every harsh setting
In every row of the table above, the elastomer fails before the brass does. That has two consequences worth building into a maintenance plan.
Specify the elastomer by name on the order. “Rubber seal” is not a specification. EPDM, NBR and silicone have different temperature ceilings and different chemical resistances, and the cheapest one on the quotation is rarely the right one.
Stock spare seals in the same compound as the fitted glands. A replacement seal of a different material is a new failure mode, and one that is invisible until the next washdown.
Where the environment is defined by a chemical rather than a temperature, the selection method — medium list, concentration, temperature and contact time — is in chemical resistant cable glands.
Specifying for harsh duty: what goes on the PO
Harsh-duty failures are frequently procurement failures. Four lines prevent most of them.
Environment, described as loads. “Coastal, wind-driven spray, ambient to 45 °C, weekly washdown with chlorinated sanitiser” — not “harsh”.
Construction. Standard or heavy-duty, with or without separate clamping, shroud included or not.
Seal compound and temperature. Named elastomer plus the peak temperature it will see, measured at the gland rather than at the room thermostat.
Thread and cable range. Thread family, size, and the measured sheath diameter range the batch must cover.
When brass is the wrong answer
Three cases should go straight past brass, whatever the plating:
Sustained temperatures above the seal limit. The body will take more than the elastomer will; once the seal is the limit, brass offers no advantage over stainless and often a lower ceiling.
Acid mist or strong oxidisers in condensate. Nickel is consumed locally and the brass underneath is attacked at the same point. Plating raises the time to failure, not the outcome.
Hygienic washdown zones in food and pharma. Caustic and chlorinated chemistry plus daily thermal cycling is a stainless application, and often a specific stainless grade rather than a generic one.
Indicative pricing
النوع
Specification
Typical application
Indicative FOB price
Standard brass
M14–M63, single seal, bare or plated
Indoor factory floor, dry plant rooms
US$0.08–1.20 per piece
Heavy-duty brass
Thicker body, separate clamping, plated, shroud
Foundry, quarry, washdown, vibration
US$0.60–4.80 per piece
Armoured brass
BW/CW/E1W with cone and earth tag
Steel plants and outdoor runs on SWA
US$1.20–7.50 per piece
Indicative FOB Ningbo/Shanghai, based on 1,000 pieces per size. Final pricing depends on size mix, plating, seal compound and order quantity.
MOQ is 1,000 pieces per size for brass with no tooling charge, and trial orders of 100–500 pieces are possible. Typical production lead time is 15–25 days depending on plating and seal compound. Representative sizes for harsh duty: M20 standard brass و M25 waterproof brass. For the material basics behind these options, see what a brass cable gland is.
Frequently asked questions
Is nickel-plated brass suitable for outdoor industrial use?
Yes, in most inland outdoor settings, particularly with a shroud. Plating raises the time to first corrosion in chloride exposure from months to years. It does not survive permanent salt spray or acid mist indefinitely, and it does not help with abrasion because the layer is thin.
Should I choose heavy-duty brass or stainless steel?
Heavy-duty brass when the loads are mechanical — impact, vibration, repeated re-tightening, abrasive dust — and the chemistry is mild. Stainless when the chemistry is the driver, especially chlorides with heat, caustic washdown, or acid condensate.
Why did my brass glands go white and rough in a washdown area?
That is dezincification, not surface dirt. The zinc leaves the alloy and leaves a porous copper-rich layer that cannot be cleaned off. It usually means the environment was beyond the plating, or the thread had already been damaged at installation.
Does a heavy-duty brass gland last longer in high temperature?
No. The temperature limit is set by the seal compound, not the body. Above the seal’s ceiling the gland fails regardless of wall thickness — use a heat-rated elastomer or a different material chain.
How many spare glands should a harsh-environment site hold?
Enough to replace the entries that get opened most often, in the sizes and finishes actually fitted — typically 5–10% of installed quantity per size. Mixed finishes and mixed seal compounds in stores are a common source of wrong-part replacement.
How to earth an armoured cable gland properly: earth tag options, contact resistance across the stack, whether the armour can be the CPC, and how to interpret the test reading.
Why 316 stainless steel cable glands fail at sea, and what the position of the entry has to do with it. Exposure zones, crevice corrosion, free iron, washdown and installation discipline.
نحن نستخدم ملفات تعريف الارتباط لتحسين تجربة التصفح الخاصة بك، وعرض إعلانات أو محتوى مخصص، وتحليل حركة المرور لدينا. بالنقر على "قبول الكل"، فإنك توافق على استخدامنا لملفات تعريف الارتباط.